

 English
 中文简体
High-Concentration Eco-Friendly Carrier for Low-Temperature Polyester Dyeing
Content
- 1 1. The Role of Carriers in Modern Textile Dyeing
- 2 2. Product Composition and Technical Profile
- 3 3. Application Areas
- 4 4. Recommended Dosage and Process Guidance
- 5 5. Corrective and Repair Applications
- 6 6. Advantages Compared with Conventional Carrier Technologies
- 7 7. Manufacturing Strengths and Technical Support
- 8 8. Environmental and Compliance Considerations
- 9 9. Storage, Handling, and Seasonal Use
- 10 10. Quality Control in the Dye House
- 11 11. Economic Value for Textile Manufacturers
- 12 12. Why Supplier Capability Matters
- 13 13. Frequently Asked Questions
- 13.1 Q1: What is the main purpose of this product?
- 13.2 Q2: Which fibers are suitable for the carrier?
- 13.3 Q3: Can it replace high-temperature polyester dyeing completely?
- 13.4 Q4: What dosage should be used?
- 13.5 Q5: Is the product compatible with all other textile auxiliaries?
- 13.6 Q6: Does the product affect light fastness?
- 13.7 Q7: Does it have a strong odor?
- 13.8 Q8: What should be done if the product crystallizes in winter?
- 13.9 Q9: Can it remove polyester oligomers?
- 13.10 Q10: What manufacturing support does the supplier provide?
- 13.11 Q11: Is this product suitable for environmentally responsible textile production?
- 13.12 Q12: Should the product be tested before bulk production?
- 14 14. Conclusion
- 15 References
- 16 Product: High-Concentration Eco-Friendly Carrier
The textile industry is under increasing pressure to reduce energy consumption, improve dyeing consistency, meet stricter environmental expectations, and maintain competitive production costs. Polyester dyeing is central to this challenge because conventional polyester dyeing commonly requires elevated temperatures, extended processing times, and carefully controlled dye dispersion. These conditions can increase energy use, intensify oligomer-related problems, and create risks such as uneven shades, dye spots, poor penetration, and machine contamination.
High-Concentration Low-Temperature Eco-Friendly Carrier is designed to address these challenges through a specialized functional structure based on a benzyl benzoate derivative. As an anionic dyeing auxiliary, it accelerates the diffusion of disperse dyes into polyester fibers, supports level dyeing, improves penetration, and helps dyeing teams achieve stable shades at reduced temperatures. The product can also be used after dyeing as a correcting agent for uneven shades, dye spots, stains, and related defects.
Its value extends beyond its role as a simple dyeing accelerator. The product combines dye diffusion, leveling, migration, dispersing, dissolving, extracting, and purifying functions in one concentrated formulation. It can help remove polyester oligomers, fiber oils, surface oils, and certain mineral residues associated with elastane-blended fabrics. It also assists in reducing back-staining and contamination within dyeing equipment.
Manufactured by Jiangyin Huanan New Materials Technology Co., Ltd., the carrier is supported by the company’s long experience in textile chemical production, research and development, laboratory testing, standardized manufacturing, and quality control. The company operates two production plants with an annual production capacity of 60,000 tons and supplies a broad range of pre-treatment, dyeing, printing, and finishing auxiliaries.
High-Concentration Eco-Friendly Carrier
1. The Role of Carriers in Modern Textile Dyeing
Carriers are functional dyeing auxiliaries that improve the movement of dye molecules toward and into hydrophobic synthetic fibers. Polyester is naturally compact and has limited affinity for many dye systems at lower temperatures. In conventional high-temperature dyeing, heat helps open the fiber structure sufficiently for disperse dyes to diffuse into the polymer matrix. However, high-temperature processing may require greater energy consumption, place additional demands on equipment, and increase the possibility of certain dyeing defects.
A suitable carrier modifies the dyeing environment and assists the transfer of dye molecules from the dye bath to the fiber. It can improve dye dispersion, facilitate fiber wetting, enhance migration, and support the penetration of dye into the fiber structure. The result is a more uniform shade and improved utilization of the dyestuff.
Traditional carriers may have disadvantages such as strong odor, high volatility, difficult handling, inadequate environmental profiles, or negative effects on fastness. Some older carrier technologies are also associated with chlorinated aromatic compounds or other substances that are increasingly unacceptable in responsible textile production. Modern mills therefore need alternatives that combine performance with improved environmental and operational characteristics.
High-Concentration Low-Temperature Eco-Friendly Carrier is formulated to provide this balance. It is intended to support low-temperature polyester dyeing while maintaining effective dye acceleration and levelness. Its functional structure promotes rapid disperse dye diffusion and provides migration properties that help minimize localized shade concentration.
1.1 Why Low-Temperature Dyeing Matters
Temperature is one of the most important variables in textile dyeing. Reducing the dyeing temperature can lower energy consumption, reduce thermal stress on fibers, support shorter production cycles, and improve process flexibility. Lower-temperature processing can be especially valuable when dyeing blended fabrics containing fibers with different thermal sensitivities.
However, simply lowering the temperature without adjusting the chemical system may lead to insufficient dye penetration, low exhaustion, poor shade development, and unacceptable levelness. A low-temperature process must therefore be supported by a properly selected carrier, suitable dispersing agents, compatible dyes, effective pH control, and an optimized heating and cooling profile.
The product helps make lower-temperature processing more practical by accelerating the diffusion of disperse dyes. At 100°C and 110°C, it can support the development of light, medium, and dark shades at dosage levels suited to the depth of shade. The exact dosage depends on the fiber type, fabric construction, dye combination, equipment, liquor ratio, and desired color strength.
1.2 The Importance of Level Dyeing
Level dyeing refers to the uniform distribution of color throughout the fabric. It is influenced by dye selection, fabric preparation, liquor circulation, temperature control, chemical compatibility, and the migration behavior of the dye. Even when all other conditions are carefully managed, some polyester dyeing systems can develop localized concentrations of dye that appear as bars, cloudy areas, streaks, or uneven depth.
A carrier with good migration properties gives dye molecules a better opportunity to redistribute during the dyeing process. This is particularly useful when the fabric has variable density, complex construction, mixed fiber content, or uneven absorbency. The product supports thorough penetration and helps reduce the risk of dyeing defects caused by insufficient movement of dye in the bath or fiber.
The leveling effect is also relevant when a mill must correct a shade that has already developed unevenly. Used under appropriate conditions, the carrier can assist in repairing shade differences, dye spots, stains, and similar defects without requiring immediate rejection or complete reprocessing of the fabric.
2. Product Composition and Technical Profile
The principal chemical composition is identified as a benzyl benzoate derivative. This functional structure is associated with the product’s ability to assist disperse dye diffusion in polyester fibers. The product is anionic in ionic character, which should be considered when evaluating compatibility with other auxiliaries, dyes, and process chemicals.
| Property | Technical information | Practical significance |
|---|---|---|
| Chemical composition | Benzyl benzoate derivative | Supports dye diffusion and carrier performance in synthetic-fiber dyeing |
| Ionicity | Anionic | Requires compatibility assessment with the complete dye-bath formulation |
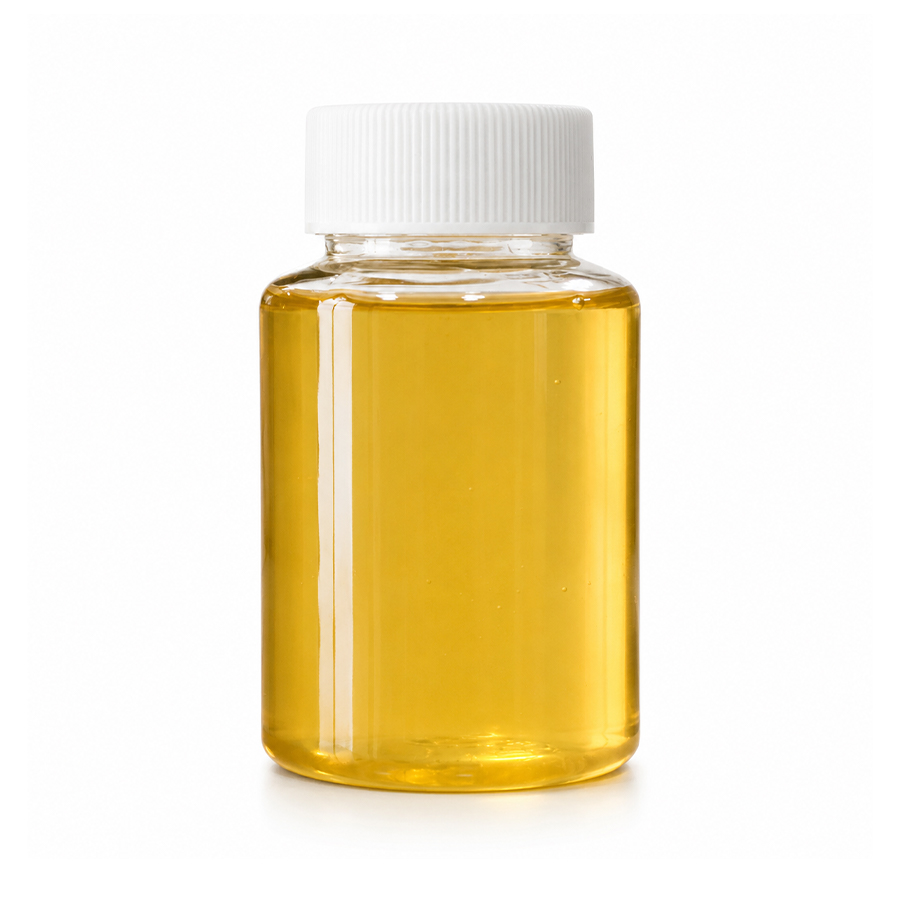
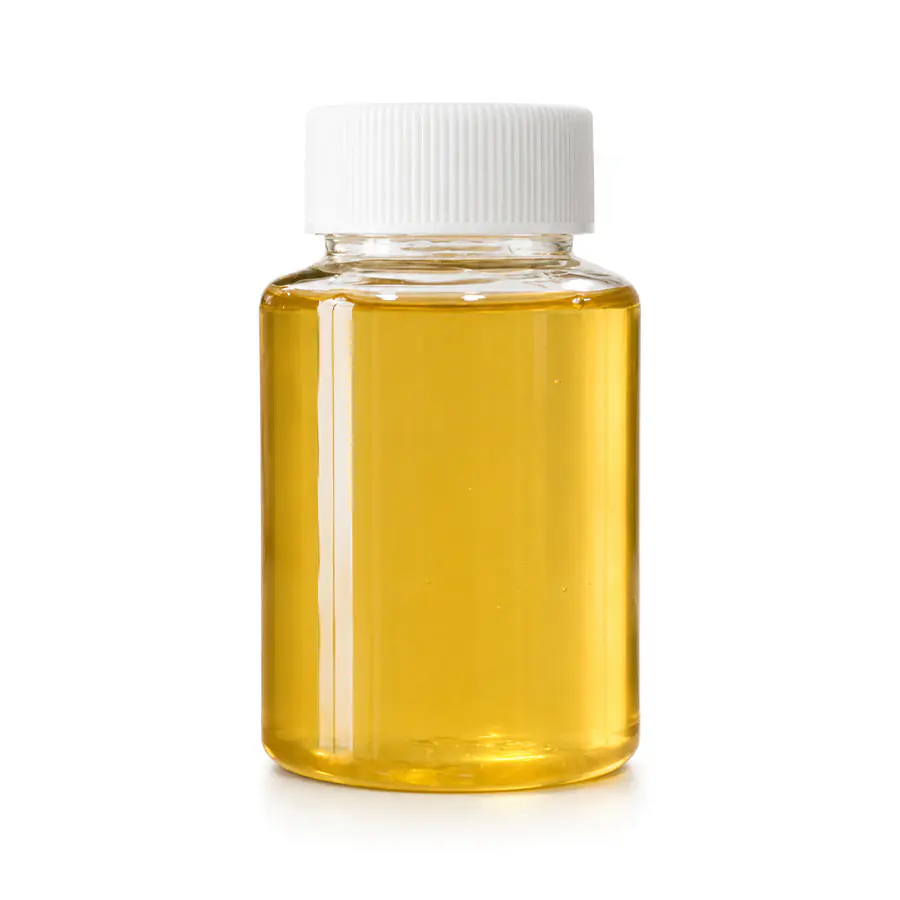
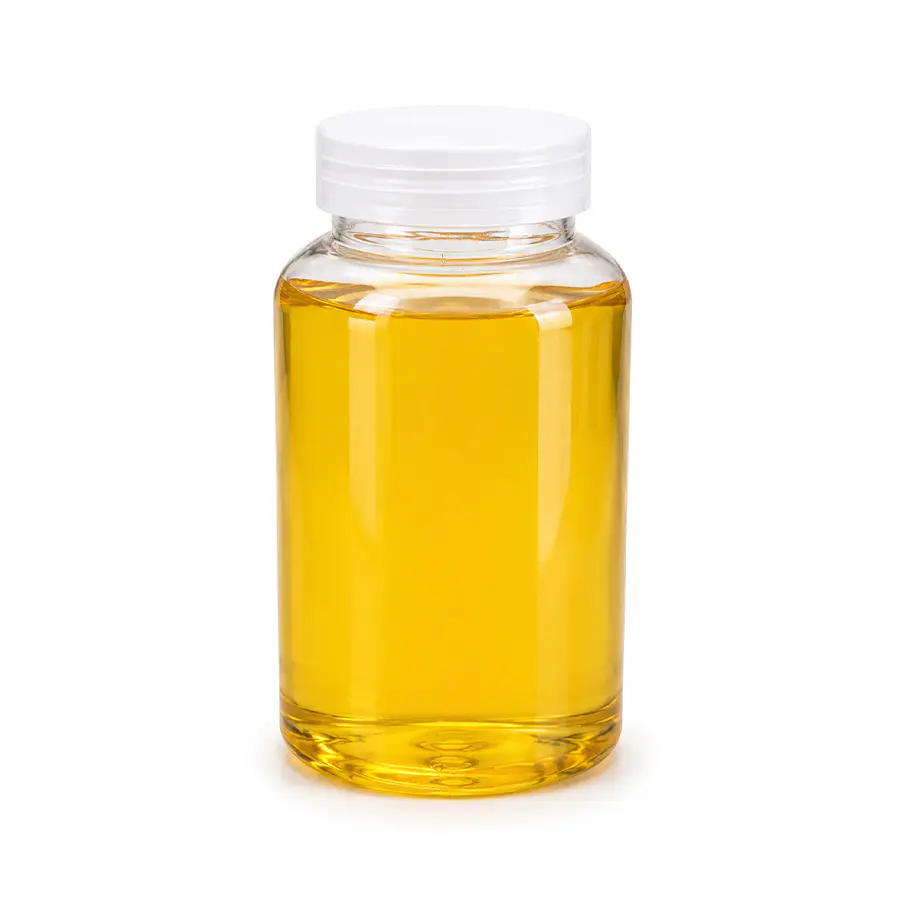
| Appearance | Light yellow transparent liquid | Convenient for visual inspection and liquid dosing |
| Solubility | Self-emulsifying upon contact with water | Supports practical preparation and dispersion in the dye bath |
| Storage life | One year under specified storage conditions | Allows planned inventory management when stored correctly |
The product is a light yellow transparent liquid and is self-emulsifying when it comes into contact with water. This property simplifies preparation compared with products that require complicated pre-emulsification procedures. Nevertheless, mills should still introduce the product gradually into a well-circulated bath and follow their established dosing procedures to achieve uniform distribution.
Self-emulsification is especially useful in production environments where chemical preparation time must be minimized. A liquid auxiliary can also be metered more easily than a solid product, supporting consistency between batches. Automated dosing systems may be used where appropriate, provided that the equipment is compatible with the product and the operating team has validated the dosing method.
2.1 Functional Performance
The product’s main function is to accelerate disperse dye diffusion into polyester fibers. This can improve the rate at which color develops and help the dye reach a more uniform distribution. It also contributes to migration, meaning that dye can move from areas of higher concentration toward areas of lower concentration during the dyeing cycle.
Its functional benefits include:
• Low-temperature dyeing support for polyester fibers.
• Rapid diffusion of disperse dyes into hydrophobic synthetic fibers.
• Improved migration and levelness.
• Better penetration through the fabric structure.
• A certain deepening and color-enhancing effect.
• Assistance in correcting uneven shades after dyeing.
• Support for the removal of polyester oligomers.
• Dispersing, dissolving, extracting, and purifying capabilities.
• Removal of fiber oils and various oils from fabric surfaces.
• Removal of certain minerals from elastane-blended fabrics.
• Reduction of back-staining.
These functions make the product relevant not only during the main dyeing stage but also during troubleshooting, corrective treatment, and process optimization.
3. Application Areas
3.1 Polyester Fibers
The primary application is the dyeing of polyester fibers with disperse dyes. Polyester fabrics are widely used in apparel, sportswear, home textiles, technical textiles, linings, knitted fabrics, woven fabrics, and blended materials. The product is suitable for mills seeking a lower-temperature route or improved dyeing stability in standard polyester processing.
In polyester dyeing, the product can improve the movement and penetration of disperse dyes. It may be particularly useful when the mill is working with difficult shades, dense constructions, deep colors, or fabrics that show a history of shade irregularity. The precise benefit depends on the total recipe and process conditions, so laboratory trials should be conducted before bulk production.
3.2 Wool and Polyester Blends
Wool and polyester blends require careful process control because the component fibers have different chemical and thermal characteristics. The polyester portion generally requires disperse dyes, while the wool portion may require an acid or metal-complex dye system. Excessive temperature or aggressive chemistry can affect the handle, appearance, or performance of the wool component.
A low-temperature carrier can support more flexible processing by promoting polyester dye diffusion at a lower temperature than would otherwise be required. The mill must still confirm compatibility with the wool dye system, pH conditions, leveling agents, and any auxiliaries used to protect the wool fiber.
3.3 Polyester and Cellulose Blends
Polyester/cellulose blends are widely used because they combine the durability and dimensional stability of polyester with the comfort and moisture characteristics of cellulose fibers. Their dyeing often involves different dye classes and may require separate or sequential dyeing stages.
The carrier is suitable for the polyester portion of such blends. Its use can help achieve a more complete and uniform disperse dyeing phase while allowing the mill to manage the cellulose component under appropriate conditions. The final recipe should consider the potential interaction between the carrier, disperse dyes, reactive dyes, direct dyes, salts, alkalis, and other process chemicals.
3.4 Triacetate Fibers
Triacetate fibers can be dyed with disperse dyes and may benefit from carefully selected dyeing accelerators. The product is suitable for triacetate applications where improved dye diffusion, shade development, and levelness are required. As with all synthetic fibers, the mill should conduct compatibility and fastness testing using the actual fiber, dye combination, and production equipment.
3.5 Modified Polyacrylic Fibers
The product is also suitable for dyeing modified polyacrylic fibers with anionic dyes. This application broadens its usefulness beyond conventional polyester dyeing. Because modified acrylic fibers can vary significantly in chemical structure and dye affinity, laboratory validation is essential for determining the best concentration, temperature profile, and auxiliary combination.
3.6 Elastane-Blended Fabrics
Elastane blends may retain mineral residues, oils, processing lubricants, or other contaminants that affect dyeing appearance and fabric performance. The product offers useful extracting and purifying functions in these systems. It can help remove certain minerals from elastane-blended fabrics and reduce the risk of back-staining.
Back-staining is a common concern in blended-fabric processing. Loose dye or contaminants may redeposit on areas of the fabric where they are not wanted, producing dullness, staining, or poor contrast. By supporting dispersion, extraction, and cleaning, the carrier can contribute to a cleaner and more stable process.
4. Recommended Dosage and Process Guidance
The recommended dosage varies according to dyeing temperature and shade depth. The following dosage ranges are based on the supplied product information and should be treated as a starting point for laboratory and production trials.
| Dyeing temperature | Shade depth | Recommended dosage |
|---|---|---|
| 100°C | Light shades | 0.5–1.0% |
| 100°C | Medium shades | 1.0–2.0% |
| 100°C | Dark shades | 2.5–3.5% |
| 110°C | Light shades | 0.3–1.0% |
| 110°C | Medium shades | 0.5–1.5% |
| 110°C | Dark shades | 1.5–2.5% |
Dosage is normally calculated based on the weight of the material, according to the mill’s standard expression for textile auxiliaries. The correct concentration should be determined through laboratory trials. Factors such as the type of polyester, fabric weight, fabric construction, dye concentration, dye combination, liquor ratio, machine design, heating rate, and required shade depth may affect the result.
4.1 Use at 100°C
At 100°C, the product can support low-temperature polyester dyeing by accelerating disperse dye diffusion. Light shades generally require a lower dosage, while dark shades may require a higher concentration to achieve sufficient color development and penetration.
Because dark shades contain a larger amount of dye and may be more sensitive to uneven migration, the recommended range at 100°C is higher than the range used for light shades. A mill should avoid assuming that the highest dosage is always the best choice. Excessive auxiliary use can alter the dye-bath balance, influence residual bath characteristics, or create unnecessary cost. Optimization should therefore be based on shade reproducibility, exhaustion, levelness, fastness, and fabric appearance.
4.2 Use at 110°C
At 110°C, the higher temperature already contributes to dye diffusion. Consequently, the recommended carrier dosage is generally lower than at 100°C. This may provide a cost advantage and help mills balance energy reduction with chemical consumption.
For a given fabric and shade, the mill may compare 100°C and 110°C processes to determine the most economical and technically reliable combination. The preferred process should be evaluated not only by immediate color development but also by final shade accuracy, washing requirements, fastness, fabric hand, machine cleanliness, and total production cost.
4.3 General Dosing Procedure
The product should be added to a well-circulated dye bath. Since it is self-emulsifying upon contact with water, it can generally be introduced into the bath in liquid form. Controlled addition is recommended, particularly in small liquor ratios or systems with limited circulation.
A practical procedure may include the following steps:
1. Confirm the fabric weight, liquor ratio, dye recipe, and target shade.
2. Prepare the dye bath with the required water and compatible auxiliaries.
3. Add the carrier under circulation and allow it to distribute uniformly.
4. Introduce the disperse dyes according to the established mill procedure.
5. Apply the programmed heating rate rather than a sudden temperature increase.
6. Maintain the selected dyeing temperature and holding time long enough to achieve the required exhaustion and penetration.
7. Cool and rinse according to the dye and fabric requirements.
8. Evaluate shade, levelness, fastness, surface cleanliness, and residual oligomer or oil-related effects.
This sequence is a general framework rather than a substitute for a validated recipe. The actual order of addition may need to be adjusted according to the machine, dye system, and other auxiliaries in use.
5. Corrective and Repair Applications
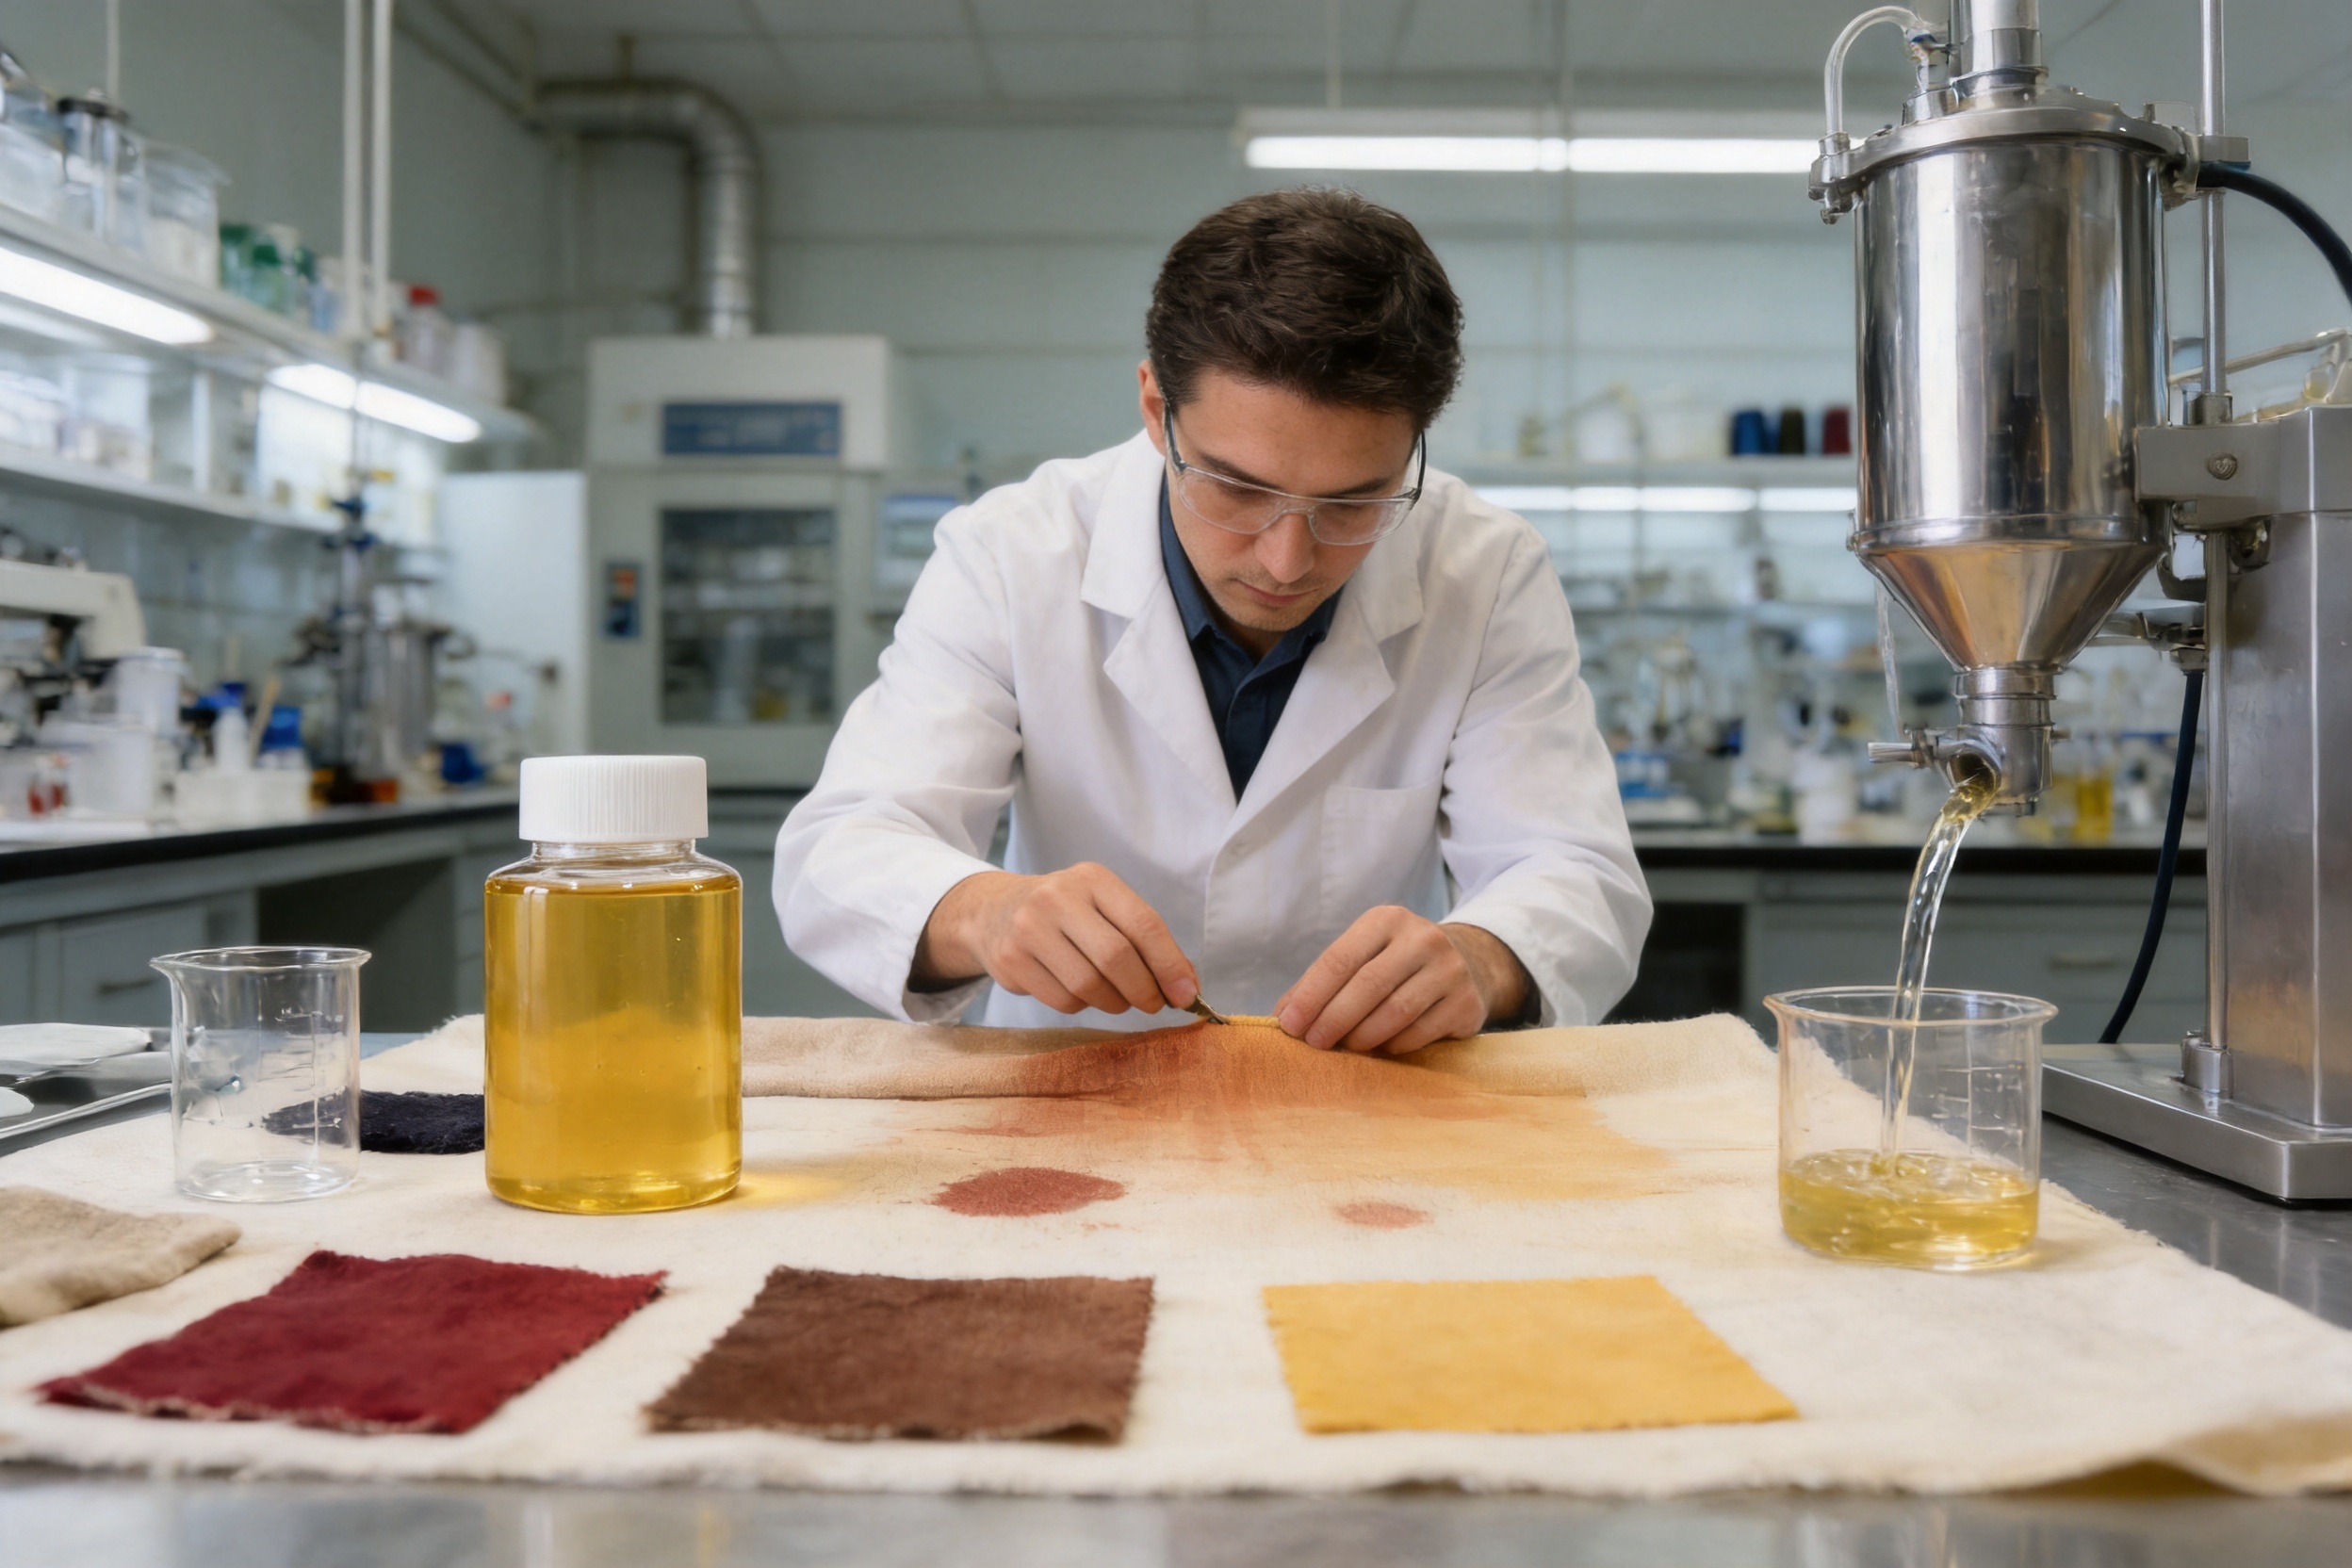
One of the product’s important advantages is its use as a correcting agent after dyeing. Dyeing mills frequently encounter shade unevenness, dye spots, stains, cloudy areas, or local differences caused by fabric preparation, circulation, dosing, temperature variation, or dye compatibility. Corrective treatment can sometimes recover material that would otherwise require stripping, redyeing, downgrading, or rejection.
The carrier’s migration and diffusion properties help redistribute color and improve the appearance of unevenly dyed material. Its use should be evaluated carefully because the success of correction depends on the cause and severity of the defect. A minor migration problem may respond well, while a chemical reaction, severe oligomer deposit, fabric damage, or permanent staining may require a different treatment.
5.1 Shade Unevenness
Shade unevenness may appear as lighter and darker areas across the width or length of a fabric. It can result from poor bath circulation, uneven pretreatment, inconsistent fabric density, rapid dye addition, or inadequate migration. A corrective treatment using the carrier may improve redistribution and reduce visible differences.
5.2 Dye Spots
Dye spots can be caused by undispersed dye, agglomeration, poor chemical preparation, or localized deposition. The product’s dispersing and dissolving capabilities can support the removal or redistribution of some spot-related deposits. The fabric should be inspected before treatment so that the mill can distinguish between loose surface dye and a permanent chemical or mechanical defect.
5.3 Stains and Surface Contamination
Oils, lubricants, and processing residues can attract dye or interfere with wetting. The product can assist in extracting fiber oils and various oils from fabric surfaces. Better removal of these materials may improve wetting, reduce localized dye uptake, and promote a cleaner final appearance.
5.4 Polyester Oligomers
Polyester oligomers are low-molecular-weight substances that can migrate from polyester fibers during dyeing. They may deposit on fabric surfaces, machine components, or internal circulation systems. Such deposits can contribute to white powder, dull areas, specks, dye spots, and machine contamination.
The product is designed to help overcome problems associated with polyester oligomers. Its dispersing, dissolving, extracting, and purifying functions can assist in keeping unwanted material mobile or removing it during the process. Good machine cleaning, correct dye-bath management, suitable rinsing, and regular maintenance remain important because no single auxiliary can replace complete process control.
6. Advantages Compared with Conventional Carrier Technologies
Textile mills may compare carriers according to their acceleration performance, levelness, odor, volatility, environmental profile, compatibility, dosage, influence on fastness, and ease of use. High-Concentration Low-Temperature Eco-Friendly Carrier offers several advantages over conventional carrier approaches.
6.1 High Concentration and Efficient Use
The product is described as a high-concentration carrier. A concentrated formulation can reduce the volume of auxiliary required per batch when compared with a more dilute product providing similar functionality. This may simplify storage, handling, transport planning, and dosing management.
High concentration does not mean that the product should automatically be used at the lowest possible dosage. The correct concentration must be established by testing because different fabrics and dyes require different levels of assistance. The key advantage is the ability to provide strong functional performance within a practical dosage range.
6.2 Lower-Temperature Capability
Conventional polyester dyeing often depends heavily on high temperatures to accelerate disperse dye penetration. The product supports dyeing at 100°C and 110°C, offering mills an alternative route where lower-temperature processing is desirable.
Lower-temperature operation may reduce energy demand and thermal stress, particularly when the process is optimized to avoid unnecessary heating and holding. It may also provide greater flexibility for blended fabrics and sensitive constructions. Actual energy savings depend on the complete production cycle, machine efficiency, liquor ratio, heating system, and cooling requirements.
6.3 Improved Migration and Levelness
Some carrier technologies accelerate dye uptake but do not provide sufficient migration. Rapid uptake without adequate redistribution can increase the risk of unlevel dyeing. This product is designed to combine acceleration with excellent migration properties, supporting a more balanced color distribution.
6.4 Low Volatility and Low Odor
The product has low volatility and low odor. These characteristics can improve the working environment and reduce concerns associated with strong-smelling carrier systems. Lower volatility can also support more stable handling and reduce the tendency of the auxiliary to escape from the process during heating.
6.5 No Chlorinated Aromatic Compounds
The product contains no chlorinated aromatic compounds, according to the supplied information. This is an important distinction from certain older carrier technologies that may raise environmental, regulatory, or brand-compliance concerns. Mills should still review the full technical documentation and perform their own compliance checks for specific market requirements.
6.6 No Damage to Light Fastness
The product is designed not to damage light fastness. Light fastness remains a critical performance property for outdoor clothing, curtains, automotive textiles, sportswear, and other products exposed to sunlight. Final performance depends on the dye class, fiber, finishing system, exposure conditions, and complete recipe, so testing should be performed on the actual product construction.
6.7 Multi-Functional Process Support
Compared with an auxiliary designed only to accelerate dyeing, this carrier provides broader functions. It supports diffusion, migration, leveling, penetration, dispersing, dissolving, extracting, and purifying. It can also assist in the removal of oils, minerals, and oligomer-related deposits.
This multi-functional profile may reduce the need to combine several separate products. Fewer products can simplify inventory, reduce dosing complexity, and make recipe control easier. However, compatibility must always be confirmed before replacing a multi-product system with a single auxiliary.
7. Manufacturing Strengths and Technical Support
The performance of a textile auxiliary depends not only on its formulation but also on manufacturing consistency. Small differences in raw materials, reaction control, blending, emulsification, filtration, storage, or packaging can influence the behavior of a carrier in the dye bath. For this reason, mills increasingly evaluate the supplier’s production capability as carefully as the product’s technical claims.
Jiangyin Huanan New Materials Technology Co., Ltd. was established in 1984 and has developed long-term experience in textile printing and dyeing auxiliaries. The company specializes in the research, development, production, and sales of pre-treatment, dyeing, and finishing auxiliaries. Its product portfolio includes moisture-wicking finishing agents, high-concentration repairing agents, low-temperature environmentally friendly carriers, silicone oils, silicone softeners, antistatic agents, color-fixing agents, stiffening agents, down-proof and windproof agents, and dry and wet rubbing fastness enhancers.
7.1 Two Production Plants
The company operates two production plants. A multi-plant structure can support production planning, capacity allocation, product specialization, and supply continuity. It also gives the manufacturer a broader operational base for serving customers with different order volumes and technical requirements.
7.2 Annual Production Capacity of 60,000 Tons
The company has an annual production capacity of 60,000 tons. This capacity indicates that it is equipped to serve regular industrial demand rather than only small laboratory or pilot requirements. For textile chemical buyers, manufacturing scale can support more reliable supply planning, repeat orders, and commercial production programs.
Capacity alone does not guarantee quality, but when combined with standardized production and strict quality control, it can provide a foundation for consistent delivery. Customers should still review product specifications, batch documentation, sample approval procedures, and quality agreements for individual projects.
7.3 In-House Laboratory and R&D Team
The company maintains an in-house laboratory and a professional research and development team. This internal technical capability is important because textile mills often require more than a standard product. They may need a carrier adjusted for a particular polyester type, dye combination, fabric construction, machine, or environmental target.
An in-house laboratory can support product testing, formulation improvement, application trials, and troubleshooting. It also allows the manufacturer to investigate performance issues in cooperation with customers. A technical supplier that understands both formulation chemistry and textile processing can provide more useful recommendations than a supplier focused only on product delivery.
7.4 Customized Formulation Capabilities
The company offers customized formulation capabilities. Customization may be relevant when a customer requires a specific ionic character, concentration, compatibility profile, odor level, environmental standard, performance balance, or application method. For example, a mill may need a carrier for a particular blended fabric or a formulation suitable for a specific dosing system.
Customized development should follow a structured process involving technical requirements, laboratory screening, fabric trials, fastness assessment, pilot production, and final approval. Such an approach helps ensure that a formulation is evaluated under conditions that reflect actual manufacturing.
7.5 Standardized Production and Quality Control
Standardized production helps reduce variation between batches. Important controls may include raw-material verification, production documentation, process monitoring, blending uniformity, appearance inspection, packaging checks, and finished-product testing. The exact internal control system should be confirmed directly with the manufacturer, but the company identifies standardized production and strict quality control as core strengths.
For a dyeing auxiliary, consistency is essential. A mill may have a carefully optimized recipe, but if the auxiliary behaves differently from batch to batch, shade reproducibility can suffer. Stable product appearance, solubility, ionic behavior, concentration, and functional performance are therefore important commercial considerations.
8. Environmental and Compliance Considerations
Environmental performance in textile chemistry involves more than one characteristic. It includes the chemical composition of the product, emissions and odor during use, wastewater behavior, energy consumption, worker exposure, packaging, transport, and compliance with customer restricted-substance requirements.
This carrier supports environmental objectives in several ways. Its low-temperature application can help reduce process energy demand. Its low volatility and low odor can improve the process environment. It contains no chlorinated aromatic compounds, according to the supplied information. It is also presented as an eco-friendly formulation suitable for customers seeking more responsible textile chemicals.
The company’s broader product positioning includes APEO-free and formaldehyde-free formulations. These features are relevant to textile manufacturers supplying brands and markets with strict chemical requirements. Each product should nevertheless be reviewed through its own technical and safety documentation because environmental status may vary by formulation.
The company supports compliance with international environmental and management expectations, including OEKO-TEX, ISO 14001, and ISO 45001-related requirements. Buyers should request current certificates, declarations, safety data, and restricted-substance information where necessary. Compliance verification is an ongoing responsibility shared by the supplier and the textile manufacturer.
8.1 Energy Reduction Through Process Optimization
A carrier that supports lower-temperature dyeing can become part of a larger energy-reduction program. The greatest benefit is achieved when the mill also optimizes liquor ratio, heating rate, insulation, machine loading, holding time, rinsing, and wastewater treatment. A chemical auxiliary should therefore be evaluated by its contribution to the total process rather than in isolation.
8.2 Waste Reduction and Reprocessing
Improved levelness and corrective capability can reduce the amount of fabric that must be stripped, redyed, downgraded, or rejected. Avoiding reprocessing can save water, steam, electricity, dyes, chemicals, and labor. It can also reduce production delays and improve delivery reliability.
The carrier’s ability to help address dye spots, stains, oligomers, and surface oils may therefore have both environmental and economic value. The extent of waste reduction depends on the mill’s defect rate, quality inspection system, recipe management, and ability to implement corrective treatment effectively.
9. Storage, Handling, and Seasonal Use
The recommended storage temperature is no higher than 30°C, with relative humidity below 50%. Containers should be kept sealed and stored in a clean, dry, and well-managed area. The product should be protected from excessive heat, contamination, and unnecessary exposure to air or moisture.
The stated shelf life is one year under the specified storage conditions. Stock should be managed according to a first-in, first-out system where practical. Before use, operators should inspect the product for unusual changes in appearance, contamination, or packaging condition.
9.1 Winter Crystallization
The product may crystallize during winter. This is described as a normal physical phenomenon and does not indicate that the product has lost its performance. If crystallization occurs, the product should be warmed before use until it returns to a suitable liquid state.
Warming should be controlled and gradual. The container should not be exposed to excessive or direct heat that could damage the packaging or create a safety risk. After warming, the product should be mixed or gently agitated as appropriate to restore uniformity before dosing.
Seasonal crystallization should be considered in inventory planning. Warehouses and production areas in cold climates may require temperature management. Mills should also allow enough time for winter material to warm before the scheduled dyeing batch begins.
10. Quality Control in the Dye House
Successful use of the carrier requires cooperation between the chemical supplier and the dye house. Before production adoption, the mill should establish a trial protocol covering fabric type, dye combination, shade depth, temperature, dosage, liquor ratio, heating rate, holding time, rinsing, and finishing.
Important evaluation criteria include:
• Shade accuracy compared with the approved standard.
• Levelness across the width and length of the fabric.
• Dye exhaustion and residual color in the bath.
• Penetration through the fabric structure.
• Color fastness, including light fastness where relevant.
• Fabric hand and physical appearance.
• Odor after drying and finishing.
• Presence of spots, stains, oligomer deposits, or back-staining.
• Machine cleanliness after repeated production cycles.
• Total chemical, energy, water, and labor costs.
A laboratory trial should be followed by a pilot or limited production trial. This is important because laboratory machines may not reproduce the circulation, loading, heating, and mechanical action of bulk equipment. A product that performs well in the laboratory should therefore be confirmed under realistic factory conditions.
10.1 Compatibility Testing
Because the product is anionic, compatibility testing is recommended when it is combined with cationic auxiliaries, certain fixing agents, softeners, or other potentially incompatible chemicals. Precipitation, turbidity, viscosity changes, or loss of dispersion may indicate an incompatibility problem.
Testing should be performed using the actual commercial products that will be used in production. Two products that appear compatible by chemical category may still behave differently because of concentration, formulation additives, water hardness, pH, or temperature.
10.2 Water Quality
Water hardness and mineral content can influence dyeing auxiliaries. Since the product may assist in removing minerals from elastane-blended fabrics, mills should still monitor incoming water quality and consider appropriate water treatment. Consistent water quality helps improve batch-to-batch reproducibility and reduces unexpected interactions.
11. Economic Value for Textile Manufacturers
The economic value of a dyeing carrier should be evaluated through total process cost rather than purchase price alone. A product with a slightly higher unit price may provide greater value if it reduces dosage, lowers temperature, shortens correction time, improves first-pass yield, or reduces machine cleaning requirements.
High-Concentration Low-Temperature Eco-Friendly Carrier may contribute to economic efficiency in several ways:
• Lower dosage compared with dilute formulations, depending on the application.
• Reduced energy requirements when dyeing at lower temperatures.
• Improved first-pass quality through better levelness and penetration.
• Reduced fabric loss caused by uneven shades, spots, or stains.
• Lower reprocessing requirements.
• More efficient handling due to its liquid form and self-emulsifying behavior.
• Potentially lower machine contamination related to oligomers and deposits.
• Greater flexibility in processing polyester and blended fabrics.
These benefits should be measured through controlled comparisons. A mill can compare a conventional process with the carrier-assisted process by tracking chemical cost per kilogram, energy consumption, processing time, first-pass yield, rework rate, wastewater characteristics, and final customer acceptance.
12. Why Supplier Capability Matters
Textile auxiliary performance is closely linked to supplier reliability. A carrier used in a large dye house must be available in consistent quality and sufficient volume. Delays, batch variation, or inadequate technical support can disrupt production even when the product itself is technically effective.
Jiangyin Huanan New Materials Technology Co., Ltd. combines long industry experience with production scale, an in-house laboratory, R&D capability, customized formulation services, and an integrated supply network. These features support long-term cooperation with textile manufacturers that require both standard products and tailored solutions.
The company’s specialization in pre-treatment, dyeing, and finishing auxiliaries also provides a broader technical context. A customer using the carrier may have related requirements for moisture management, softening, antistatic performance, color fixing, stiffness, down-proofing, windproofing, or rubbing fastness. Access to a wider product portfolio can make it easier to coordinate chemical solutions across several stages of textile processing.
Long-term partnerships are especially valuable when a mill is moving toward lower-temperature dyeing, more environmentally responsible chemistry, or customized production. The supplier can help with trial design, dosage adjustment, compatibility checks, defect analysis, and process refinement.
13. Frequently Asked Questions
Q1: What is the main purpose of this product?
The main purpose is to accelerate the diffusion of disperse dyes into polyester fibers during low-temperature dyeing. It also improves migration, levelness, penetration, and shade development. In selected applications, it can be used as a corrective agent after dyeing.
Q2: Which fibers are suitable for the carrier?
It is suitable for polyester fibers, wool blends, polyester/cellulose blends, triacetate fibers dyed with disperse dyes, and modified polyacrylic fibers dyed with anionic dyes. It can also be useful in elastane-blended fabrics where mineral, oil, or back-staining issues need to be addressed.
Q3: Can it replace high-temperature polyester dyeing completely?
The product is designed to support low-temperature dyeing at 100°C and 110°C, but the complete process must be validated for each fabric and shade. Dye type, polyester structure, fabric construction, machine performance, and fastness requirements all affect the suitable temperature.
Q4: What dosage should be used?
At 100°C, the recommended dosage is 0.5–1% for light shades, 1–2% for medium shades, and 2.5–3.5% for dark shades. At 110°C, the recommended dosage is 0.3–1% for light shades, 0.5–1.5% for medium shades, and 1.5–2.5% for dark shades. These ranges are for reference and should be optimized through trials.
Q5: Is the product compatible with all other textile auxiliaries?
Compatibility cannot be assumed for every formulation. Because the product is anionic, mills should test it with cationic products and other auxiliaries that may interact with anionic systems. Laboratory testing using the actual commercial products is recommended.
Q6: Does the product affect light fastness?
The supplied technical information states that it does not damage light fastness. Final light-fastness performance also depends on the dye, fiber, finishing system, exposure conditions, and complete process, so testing should be conducted on the finished fabric.
Q7: Does it have a strong odor?
The product is described as low in odor and low in volatility. This can provide a more comfortable working environment than some conventional carrier technologies with stronger odor or higher volatility.
Q8: What should be done if the product crystallizes in winter?
Winter crystallization is a normal physical phenomenon. The product should be warmed before use until it returns to a suitable liquid state. This does not affect performance when the product is properly restored and mixed before dosing.
Q9: Can it remove polyester oligomers?
The product is designed to help overcome polyester oligomer problems and has dispersing, dissolving, extracting, and purifying capabilities. It can assist with oligomer-related white powder, dye spots, deposits, and machine contamination, although regular machine cleaning and suitable rinsing remain necessary.
Q10: What manufacturing support does the supplier provide?
The supplier provides research and development, laboratory support, customized formulation capabilities, standardized production, quality control, and an integrated supply network. It operates two production plants with an annual production capacity of 60,000 tons.
Q11: Is this product suitable for environmentally responsible textile production?
The product is presented as an eco-friendly, low-temperature carrier with low volatility, low odor, and no chlorinated aromatic compounds. Lower-temperature dyeing may also help reduce energy use. Buyers should review current technical, safety, and compliance documentation for their specific market and certification requirements.
Q12: Should the product be tested before bulk production?
Yes. Laboratory and pilot trials are recommended before bulk production. Testing should cover shade, levelness, fastness, fabric hand, exhaustion, machine cleanliness, compatibility, and the total process cost.
14. Conclusion
High-Concentration Low-Temperature Eco-Friendly Carrier is a versatile auxiliary for modern polyester and synthetic-fiber dyeing. Its benzyl benzoate derivative structure, anionic character, self-emulsifying behavior, and liquid form support practical use in industrial dye houses. The product accelerates disperse dye diffusion, improves migration and levelness, supports thorough penetration, and offers a certain deepening and color-enhancing effect.
Its application range includes polyester, wool blends, polyester/cellulose blends, triacetate, modified polyacrylic fibers, and elastane-containing materials. Beyond its primary dyeing function, it helps address polyester oligomers, white powder, dye spots, stains, fiber oils, surface oils, mineral residues, and back-staining.
Compared with conventional carrier approaches, its principal advantages include low-temperature performance, high concentration, low volatility, low odor, no chlorinated aromatic compounds, support for light-fastness protection, and multi-functional process assistance. These advantages can help mills improve product quality while pursuing lower energy use, reduced reprocessing, and more responsible chemical management.
The product is supported by a manufacturer with a long history in textile auxiliaries, two production plants, an annual capacity of 60,000 tons, an in-house laboratory, professional R&D resources, customized formulation capabilities, standardized production, and strict quality control. This combination of product performance and manufacturing strength makes the carrier suitable for textile manufacturers seeking reliable, scalable, and technically adaptable dyeing solutions.
As with all textile chemicals, the best results depend on proper testing and process optimization. Mills should select the dosage according to shade depth and dyeing temperature, verify compatibility with the complete recipe, assess the finished fabric under realistic production conditions, and maintain suitable storage and handling practices. When integrated into a controlled dyeing system, the carrier can become an important tool for improving polyester dyeing quality, efficiency, and environmental performance.
References
1. Product technical information for High-Concentration Low-Temperature Eco-Friendly Carrier, including composition, properties, applications, dosage, storage, and handling guidance.
2. Jiangyin Huanan New Materials Technology Co., Ltd. Company information concerning textile auxiliary manufacturing, research and development, production capacity, customized formulation, and quality control.
3. General technical principles of disperse dyeing for polyester and other hydrophobic synthetic fibers.
4. General textile dyeing practice concerning leveling, migration, dye diffusion, oligomer control, back-staining, and corrective treatment.
5. General environmental management principles for textile chemical production and textile wet processing.
Product: High-Concentration Eco-Friendly Carrier
Contact us
huanannewmaterials@gmail.com
-
 Phone: +86 - 13861620767
-
 Fax: +86-0510-86200939
-
 298 Hongxing Road, Huashi Town, Jiangyin City, Wuxi City, Jiangsu Province, China
Product links
Mobile App
Copyright © Jiangyin Huanan New Materials Technology Co., Ltd. All Rights Reserved
-
huanannewmaterials@gmail.com
-
-
-
+86 - 13861620767