

 English
 中文简体
Advanced Down-Proof and Wind-Proof Finishing for Pure Cotton Fabrics
Content
- 1 1. The Functional Challenge: Combining Cotton Comfort with Barrier Performance
- 2 2. Product Composition and Technical Profile
- 3 3. How the Polymer Film Delivers Down-Proof Protection
- 4 4. Key Advantages Compared with Conventional Finishing Approaches
- 5 5. Recommended Application Process
- 6 6. Manufacturing Strengths Behind the Product
- 7 7. Environmental and Compliance Considerations
- 8 8. Product Advantages for Textile Manufacturers
- 9 9. Quality Evaluation and Recommended Testing
- 10 10. How the Product Compares with Alternative Strategies
- 11 11. Practical Troubleshooting Guide
- 12 12. Storage, Handling, and Packaging
- 13 13. Applications in Finished Textile Products
- 14 14. Why Supplier Collaboration Matters
- 15 15. Recommended Implementation Plan for a Textile Mill
- 16 16. Questions and Answers
- 16.1 Q1: What is the primary function of this finishing agent?
- 16.2 Q2: Can it be used on pure cotton fabrics?
- 16.3 Q3: What is the recommended dosage?
- 16.4 Q4: Which auxiliaries are compatible with the product?
- 16.5 Q5: Will the finish make cotton fabric stiff?
- 16.6 Q6: Does it affect fabric color or whiteness?
- 16.7 Q7: Can it be used with waterproof finishes?
- 16.8 Q8: What is the recommended process flow?
- 16.9 Q9: What air permeability can be expected?
- 16.10 Q10: How should the product be stored?
- 16.11 Q11: What makes the product suitable for industrial textile production?
- 16.12 Q12: Should the product be tested after laundering?
- 17 17. Conclusion
- 18 References
- 19 Product: Down-Proof & Wind-Proof Finishing Agent (Pure Cotton)
Pure cotton remains one of the most important textile fibers because of its softness, breathability, moisture absorption, comfort, and natural appearance. However, cotton fabrics can present technical challenges when they are used in down jackets, quilted garments, bedding, outdoor products, and other articles that require protection against feather leakage and wind penetration. The open structure of a woven or knitted fabric may allow small down fibers and feather shafts to pass through. At the same time, excessive air permeability can reduce warmth and compromise the performance of a finished garment.
Down-proof and wind-proof finishing provides a practical way to improve these properties without replacing the cotton substrate or fundamentally changing the fabric construction. The Down-Proof & Wind-Proof Finishing Agent for Pure Cotton is a specialized high-molecular polymer complex designed to form a dense, cross-linked film on the surface of textile fibers. This film helps close microscopic gaps within the fabric structure, reducing air movement and limiting the migration of down and feather materials.
The finishing agent is formulated to provide functional protection while preserving the softness and natural handle expected from cotton. It is suitable for pure cotton and selected cotton-blended fabrics and can be incorporated into a padding, setting, and calendering process. With a recommended application range of 50–200 g/L, the product can be adjusted according to yarn count, fabric density, construction, and performance requirements.
Manufactured by Jiangyin Huanan New Materials Technology Co., Ltd., the product reflects the company’s broader capabilities in textile auxiliary research, formulation development, production, quality management, and application support. The manufacturer operates production plants with a reported annual capacity of 60,000 tons and supplies a wide range of pretreatment, dyeing, and finishing auxiliaries for textile producers.
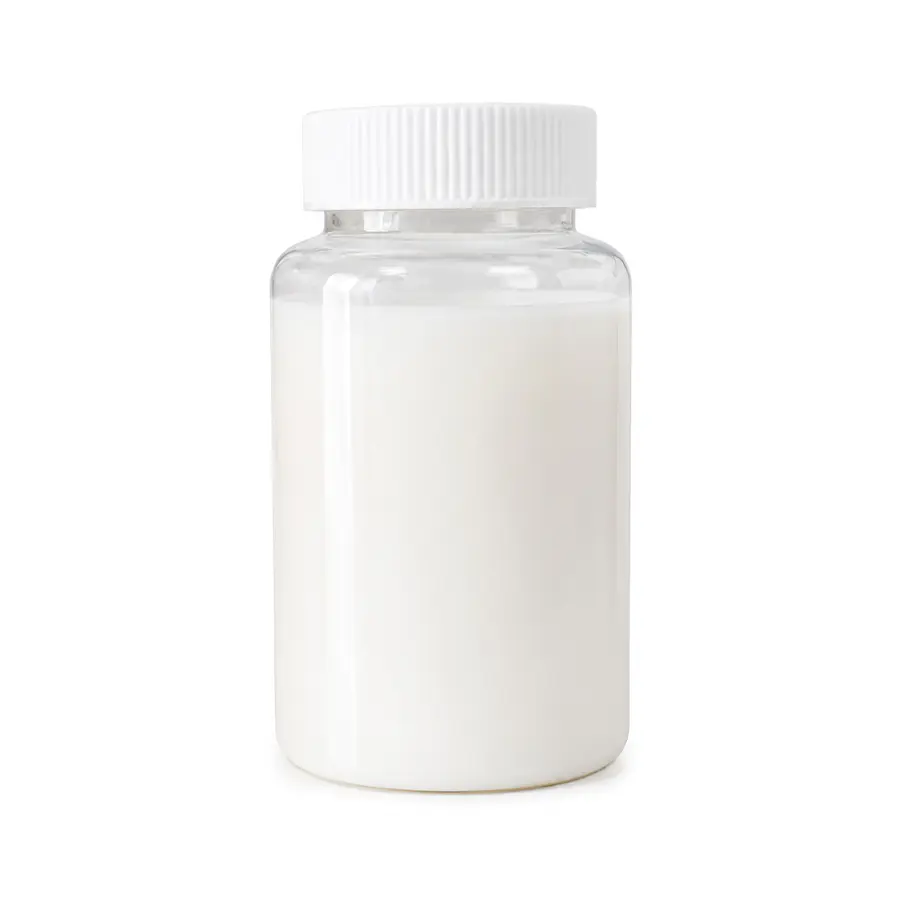
Down-Proof & Wind-Proof Finishing Agent (Pure Cotton)
1. The Functional Challenge: Combining Cotton Comfort with Barrier Performance
Down-proof fabric must perform more than one function. It needs to prevent loose down from emerging through the fabric, reduce wind penetration, maintain an attractive appearance, and preserve the original comfort of the textile. These requirements can be difficult to balance because a treatment that creates a highly impermeable film may also make the fabric stiff, plastic-like, noisy, or uncomfortable.
Pure cotton presents a particularly interesting challenge. Cotton fibers are hydrophilic and naturally absorbent, while cotton fabrics often have a relatively open and flexible structure. These characteristics provide comfort and breathability, but they may also create pathways through which air and fine feather particles can move. A suitable finishing agent must therefore provide controlled surface coverage rather than simply producing a thick, rigid coating.
The performance objective is not necessarily to seal the fabric completely. Complete sealing could negatively affect moisture management, handle, drape, and wearing comfort. Instead, the objective is to reduce the effective air permeability and close the pathways that allow down to poke through. The polymer film must be continuous enough to improve barrier performance but flexible enough to move with the textile during wear, laundering, folding, and processing.
The Down-Proof & Wind-Proof Finishing Agent addresses this requirement through a special high-molecular polymer complex. During finishing and subsequent thermal processing, the product forms a dense cross-linked film around and between the fibers. This film helps stabilize the surface structure and reduces the size and continuity of the openings through which air and down may pass.
2. Product Composition and Technical Profile
The product is supplied as a milky white to off-white emulsion. Its main component is described as a special fatty compound, and its ionic character is weakly cationic. The pH of a 1% aqueous solution is approximately 6, providing a mildly acidic working environment that is generally suitable for many textile finishing processes when the overall recipe is properly controlled.
The emulsion is easily dispersible in water, which supports convenient preparation of padding liquors. Good dispersibility is important because an unevenly prepared bath can lead to inconsistent deposition, streaks, localized stiffness, or variation in down-proof performance across the fabric width. Operators should add the product gradually under suitable agitation and confirm that the bath remains uniform before production begins.
| Property | Typical description | Practical significance |
|---|---|---|
| Appearance | Milky white to off-white emulsion | Allows visual checking of product condition before use |
| Main component | Special fatty compound | Supports flexible film formation and surface protection |
| Ionicity | Weakly cationic | Requires compatibility control when combined with other auxiliaries |
| pH value | Approximately 6 at 1% aqueous concentration | Provides a mildly acidic application environment |
| Solubility and dispersion | Easily dispersible in water | Facilitates preparation of padding baths |
| Compatibility | Compatible with non-ionic and weakly cationic auxiliaries | Supports combination finishing when bath compatibility is confirmed |
| Incompatibility warning | Do not use in the same bath with anionic auxiliaries | Prevents precipitation, instability, and uneven application |
The weakly cationic nature of the product is an important consideration in production planning. It can be used with non-ionic and weakly cationic auxiliaries, including selected softeners and other finishing products. However, it should not be mixed in the same bath with anionic auxiliaries. Ionic incompatibility may cause flocculation, precipitation, bath instability, poor exhaustion, or deposits on the fabric.
For this reason, textile mills should review the complete chemical recipe before production. If an anionic product is required for a separate stage, the processes should be separated, or a laboratory compatibility test should be completed before any scale-up. Water quality, bath temperature, agitation, addition order, and machine cleanliness can also influence formulation stability.
3. How the Polymer Film Delivers Down-Proof Protection
The central working principle is the formation of a dense cross-linked film on the fiber surface. When the treated fabric passes through the padding and thermal finishing stages, the polymer complex is distributed over the yarns and fibers. Subsequent setting and calendering help consolidate the film and improve the uniformity of the finished surface.
A down-proof effect depends on several related mechanisms. First, the film reduces the size of openings at the surface of the yarns. Second, it helps bind or stabilize loose fibers that might otherwise create channels through the fabric. Third, it provides a smoother and more continuous barrier around the individual fibers. Fourth, it reduces the force of air passing through the textile, which also decreases the likelihood that fine down fibers will be pushed through the construction.
The product is not intended to replace proper fabric engineering. Yarn count, weave density, fabric weight, finishing tension, and the condition of the fabric all influence the final result. Instead, the agent acts as a performance-enhancing finish that helps a suitable textile construction achieve improved windproof and anti-down properties.
The reported air permeability range for treated fabrics is approximately 20–30 under the relevant testing conditions, while the anti-down performance can reach below 12 counts. Exact values depend on the test method, fabric construction, dosage, drying and setting conditions, calendering pressure, and the selected softener package. Mills should therefore establish their own internal test correlation before making production guarantees.
4. Key Advantages Compared with Conventional Finishing Approaches
4.1 Improved Windproof Performance
One of the principal advantages of this finishing agent is its ability to reduce air permeability and improve protection against wind. The dense polymer film restricts uncontrolled airflow through the textile structure, helping the finished fabric provide better thermal protection in garments and quilted products.
Windproof performance is especially valuable in outerwear, lightweight jackets, sleeping products, and cotton-blended materials used in transitional or cold-weather applications. A fabric that allows excessive air exchange may feel cold even when the filling material provides adequate insulation. By reducing air penetration, the finish helps the textile contribute more effectively to the overall performance of the product.
4.2 Effective Anti-Down Performance
Down and feather leakage is a visible and functional defect. Small feather components emerging through the outer shell can cause consumer complaints, reduce garment appearance, and weaken confidence in product quality. The polymer film helps reduce these pathways and supports a cleaner, more stable surface.
The product is designed specifically for down-proof and wind-proof finishing rather than being a general-purpose stiffening agent. This specialization allows the formulation to focus on controlled film formation, flexibility, and barrier performance. When applied at an appropriate concentration and combined with suitable calendering, it can help fabrics reach demanding anti-down targets.
4.3 Soft Handle and Limited Effect on Fabric Feel
A common concern with barrier finishes is loss of softness. Heavy coatings may make fabric boardy, harsh, sticky, or excessively compact. The product is designed to form a soft film that does not significantly damage the original hand feel when the process is properly controlled.
The final handle depends on the dosage, fabric type, drying temperature, calendering pressure, and the choice of accompanying softener. The recommended application range of 50–200 g/L provides flexibility for adjustment. Lower concentrations may be suitable for tightly constructed fabrics or moderate performance targets, while higher concentrations may be considered for more open constructions or stricter barrier requirements.
4.4 Minimal Influence on Shade and Whiteness
Many textile finishers need to improve function without changing the visual appearance of the fabric. Excessive yellowing, dulling, or shade shift can create rework and compromise brand requirements. The product is designed to have minimal impact on shade and whiteness, making it suitable for colored, white, and light-colored cotton textiles when the complete recipe is compatible.
Color evaluation should nevertheless be performed after finishing. The visual result can be affected by other components in the bath, thermal exposure, optical brighteners, residual alkali, fabric preparation, and the original dye class. A laboratory trial remains the best way to confirm shade stability for a particular article.
4.5 No Intended Reduction in Waterproof Performance
The product is also described as having no adverse effect on waterproof performance. This is useful for fabrics that combine windproof and anti-down requirements with water-repellent or waterproof treatments. In practical production, the compatibility of the complete formulation must be confirmed, particularly when a hydrophobic agent, cross-linking system, or membrane-related finish is also present.
The order of application may influence the result. In some production systems, down-proof finishing may be combined with selected softeners; in others, water-repellent treatment may be applied in a separate stage. The most reliable process should be selected through laboratory trials that measure air permeability, down-proof performance, water resistance, handle, and appearance together.
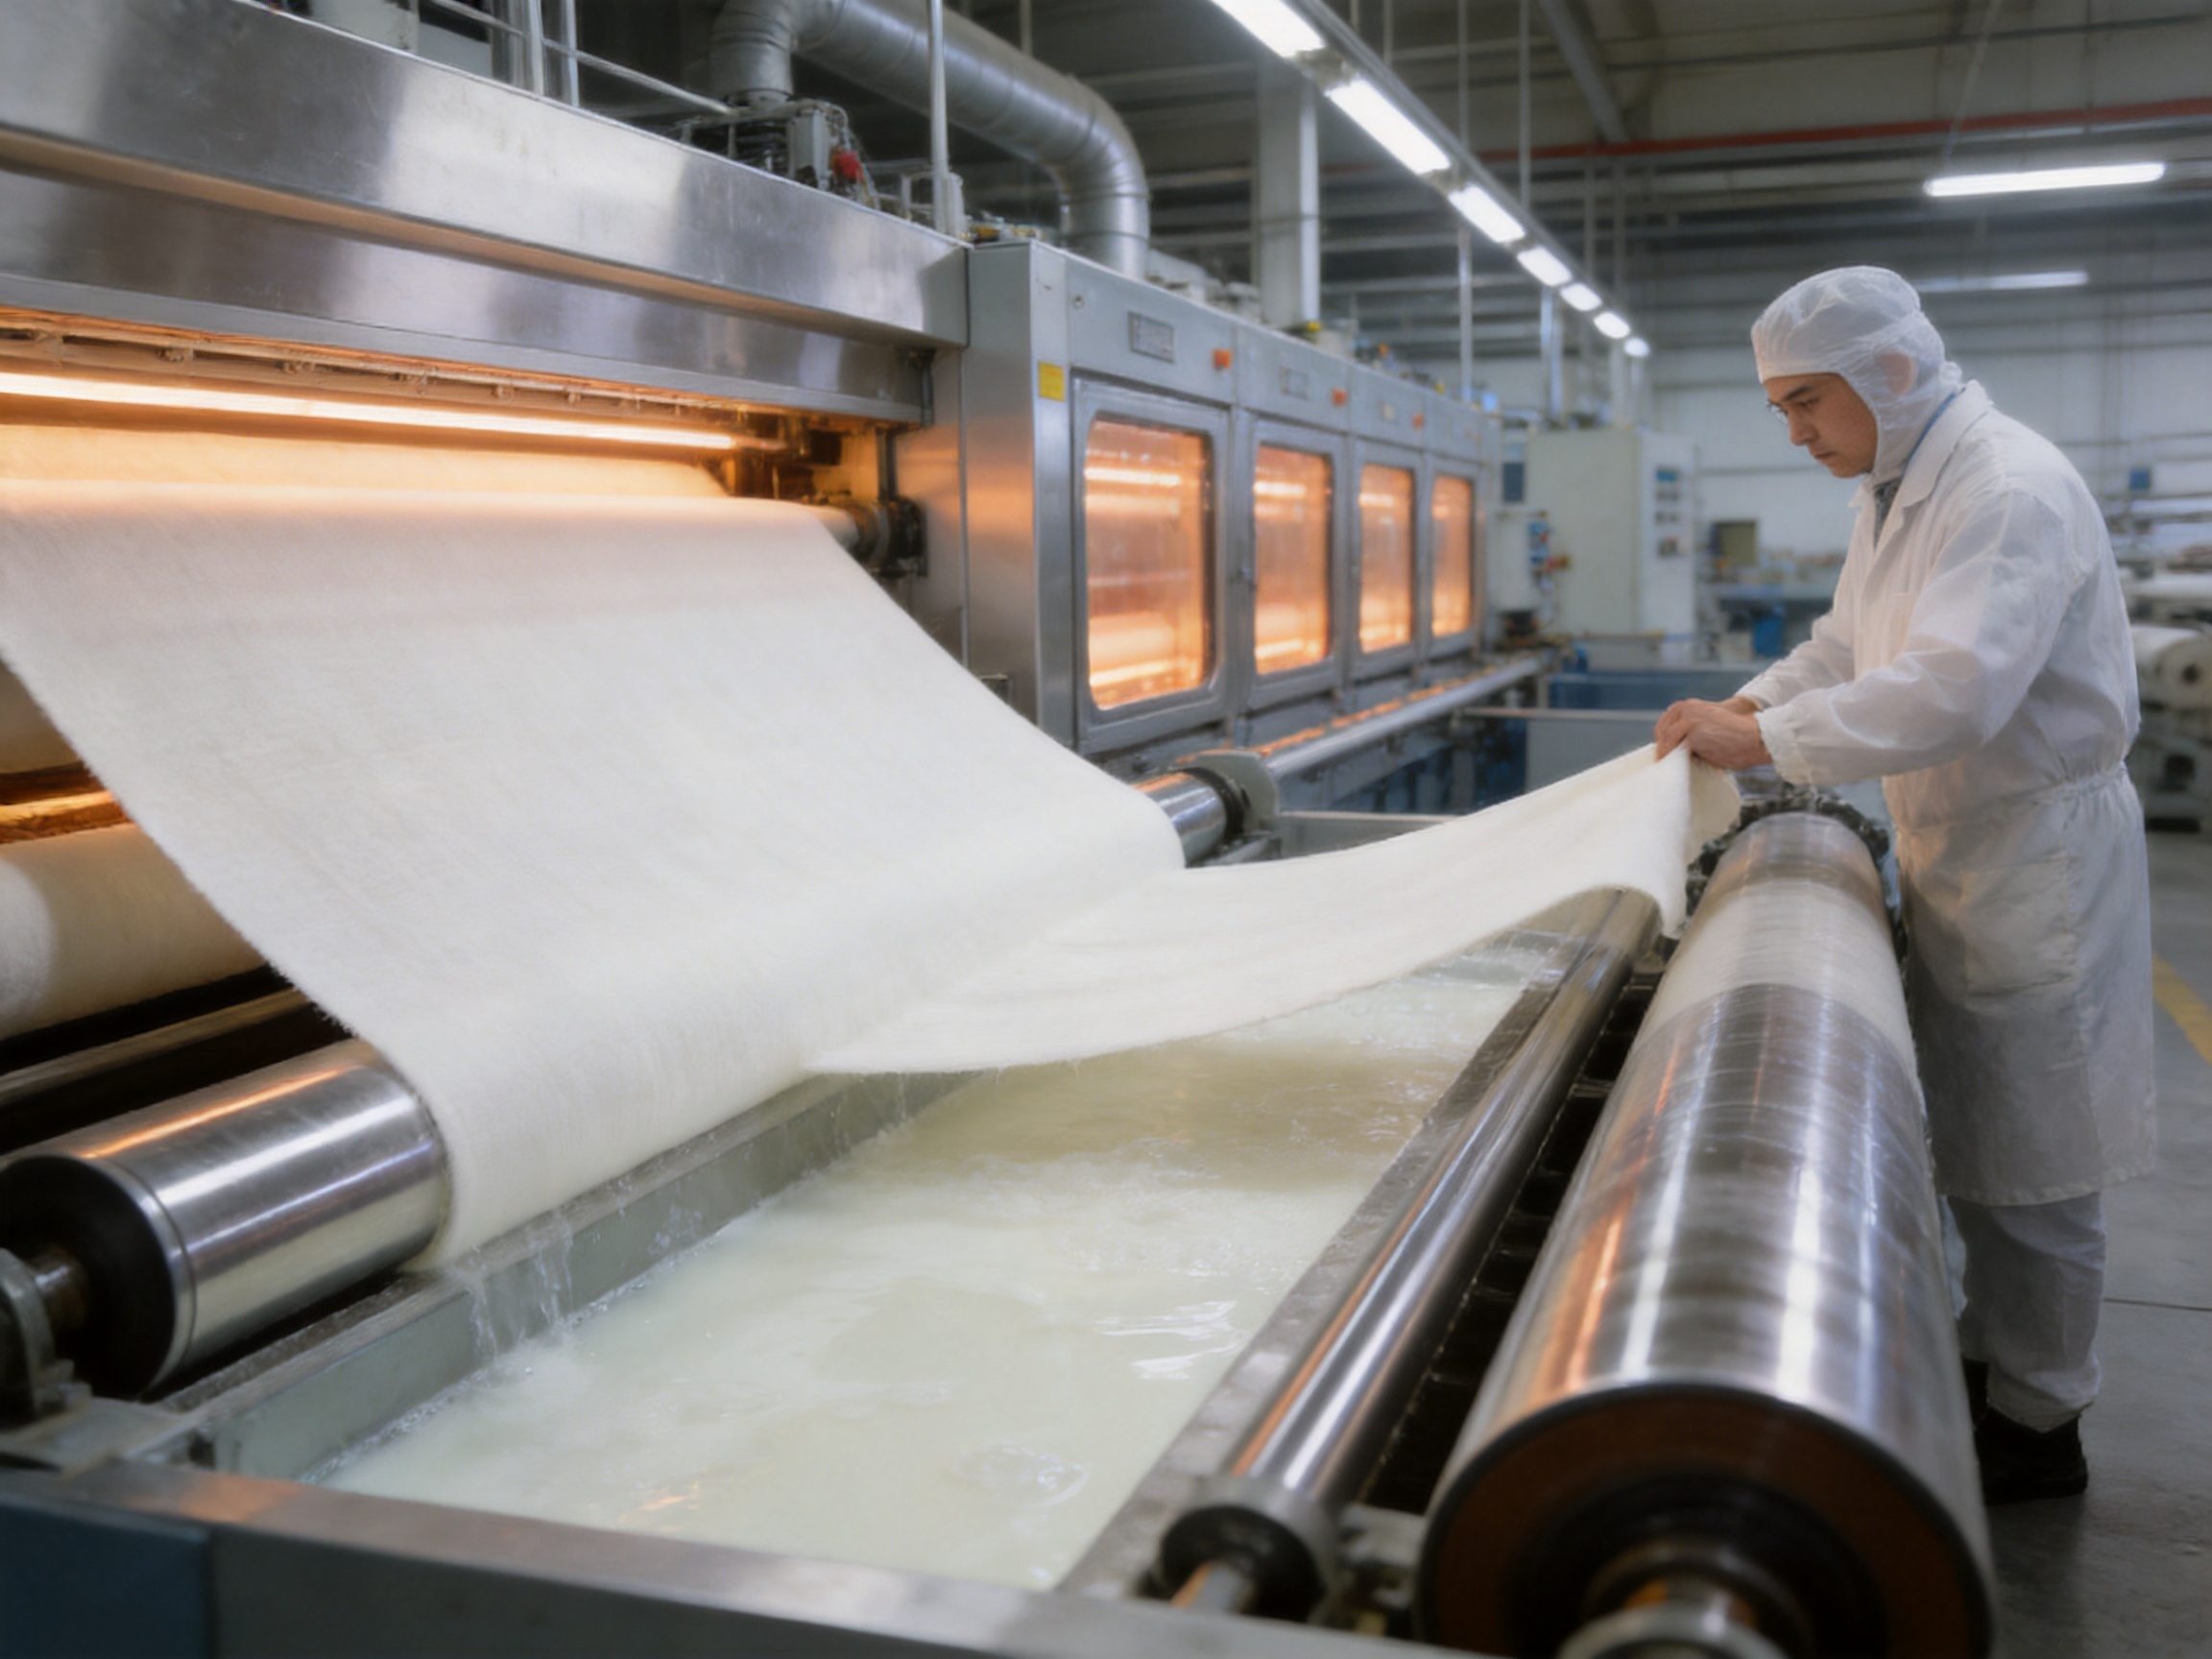
5. Recommended Application Process
The recommended application method is padding. A typical starting dosage is 50–200 g/L, with the precise concentration determined by yarn count, fabric density, fabric weight, construction, and the required performance level.
A typical process sequence is:
Padding with dry fabric feeding, using 50–200 g/L of the down-proof agent and adding softener or other compatible auxiliaries as required.
Setting under conditions appropriate for the fabric and the selected chemical recipe.
Calendering one or two times, with an approximate calendering pressure of 10 and roller temperature of approximately 80–90°C.
The stated conditions should be treated as practical starting points rather than universal fixed values. Every textile mill should optimize wet pickup, drying rate, setting temperature, line speed, calender nip pressure, roller temperature, and number of passes for the actual fabric. A process developed for a dense cotton sateen may not be appropriate for a lightweight plain weave or cotton-polyester blend.
5.1 Bath Preparation
Before preparing the padding bath, the operator should confirm the cleanliness of the tank, pipes, dosing system, padding trough, and rollers. Residues of incompatible anionic auxiliaries can destabilize a weakly cationic product. Equipment should be adequately rinsed when changing from another chemical system.
Water should be added to the preparation vessel first, followed by gradual addition of the product under moderate agitation. If other compatible auxiliaries are required, they should be introduced according to a validated addition sequence. The mixture should be observed for signs of coagulation, floating particles, excessive foam, or viscosity change.
The bath should remain adequately agitated during production, but excessive shear or air incorporation should be avoided if these cause foaming. The prepared liquor should be used within the planned production period, and the operator should monitor concentration and appearance during long runs.
5.2 Padding and Wet Pickup
Uniform padding is essential to consistent down-proof performance. Uneven wet pickup can create areas with insufficient polymer deposition and other areas with excessive film formation. The padding pressure, roller condition, fabric tension, speed, and bath level should be kept stable.
Dry fabric feeding is recommended in the stated process flow. The fabric should be properly prepared, free from excessive surface contamination, and adequately scoured or dyed according to the article specification. Any residual oils, waxes, sizing materials, or incompatible chemical deposits may interfere with film formation.
Wet pickup should be recorded because it directly affects the amount of active finish deposited on the fabric. A dosage expressed in grams per liter does not by itself define the final add-on. The actual finish level depends on bath concentration and wet pickup. Production teams should therefore calculate and monitor the theoretical add-on and verify the result through fabric testing.
5.3 Setting and Thermal Development
Setting helps stabilize the treated fabric and supports the development of the polymer film. The appropriate temperature and residence time depend on the substrate, fabric width, machine type, moisture content, and the presence of other auxiliaries. Excessive heat may affect shade, whiteness, handle, or dimensional stability, while insufficient thermal treatment may prevent the finish from developing its intended performance.
Temperature uniformity across the machine width is important. Variations in drying or setting conditions can result in inconsistent air permeability or anti-down performance from selvedge to center. Regular machine calibration and temperature mapping can help reduce this risk.
5.4 Calendering
Calendering is a significant part of the recommended process. One or two passes at an approximate pressure of 10 and a roller temperature of 80–90°C can help smooth and compact the fabric surface. The mechanical action can improve the continuity of the polymer film and reduce the size of surface openings.
Calendering also affects luster, thickness, hand feel, drape, and fabric width. Excessive pressure may create an undesired glossy appearance or overly compact handle. Insufficient pressure may leave the surface too open to achieve the required barrier performance. The best result is normally established by comparing several pressure and temperature combinations in a controlled trial.
6. Manufacturing Strengths Behind the Product
The performance of a textile auxiliary depends not only on its chemical concept but also on the consistency of its manufacture. Small variations in emulsion stability, active content, particle distribution, viscosity, pH, or raw material quality can affect production results. A reliable supplier must therefore combine formulation knowledge with disciplined manufacturing systems.
Jiangyin Huanan New Materials Technology Co., Ltd. was established in 1984 and is located in Jiangyin City, Jiangsu Province, China. The company specializes in the research, development, production, and sale of textile printing and dyeing auxiliaries. Its product portfolio includes pretreatment auxiliaries, dyeing auxiliaries, finishing agents, moisture-wicking products, repairing agents, low-temperature carriers, silicone oils, silicone softeners, antistatic agents, color-fixing agents, stiffening agents, down-proof and windproof agents, and dry and wet rubbing fastness enhancers.
The company reports two production plants and an annual production capacity of 60,000 tons. This scale supports regular supply for textile mills while retaining a product-development structure focused on specialized textile applications. Production capacity is particularly important for customers who need consistent deliveries across multiple seasons or require a formulation to remain available for repeat orders.
6.1 Research and Development Capability
Down-proof finishing involves several performance variables that cannot be optimized through a single laboratory measurement. A successful product must balance film formation, softness, compatibility, appearance, air permeability, and anti-down performance. The manufacturer’s in-house laboratory and professional research and development team support this type of multi-factor development.
Laboratory development can include screening of raw materials, adjustment of polymer structure, evaluation of emulsion stability, analysis of compatibility with softeners, and testing on different cotton constructions. Application specialists can also compare padding conditions, setting conditions, and calendering variables to identify the most suitable process window.
This development approach is advantageous for textile producers because the same chemical may behave differently on a compact poplin, a brushed cotton fabric, a lightweight plain weave, or a cotton-polyester blend. A supplier with formulation and application experience can help customers adapt the product rather than relying only on a fixed generic recipe.
6.2 Process Control and Batch Consistency
Industrial textile production requires repeatability. A fabric buyer expects the same chemical to deliver comparable performance from one batch to another, provided the substrate and process remain stable. Batch consistency depends on controlled raw material storage, accurate weighing, defined mixing procedures, temperature management, filtration, filling control, and documented quality inspection.
For an emulsion-based finishing agent, physical stability is especially important. The product should remain uniform during storage and transport, disperse readily in water, and perform consistently after preparation. Routine checks of appearance, pH, viscosity, density, and dispersion behavior can help identify deviations before the product reaches the customer.
The manufacturer’s integrated production and quality-control structure is intended to support stable delivery and predictable application. Textile mills should still carry out incoming inspection according to their own quality systems, particularly when introducing the product to a new fabric range.
6.3 Custom Formulation and Technical Support
Different markets and textile articles require different balances of properties. Some customers prioritize the lowest possible air permeability. Others place greater emphasis on softness, whiteness, low-temperature processing, water repellency, or compatibility with an existing finishing line. A standard product can provide a useful starting point, but customized formulation or process adjustment may be necessary for demanding applications.
Jiangyin Huanan’s stated customized formulation capabilities allow the company to work with customers on product adaptation and application requirements. This may involve adjusting concentration, film flexibility, compatibility, deposition behavior, or performance targets. Technical cooperation is particularly valuable when a customer is changing fabric construction, introducing recycled fibers, reducing energy consumption, or seeking an APEO-free and formaldehyde-free solution.
7. Environmental and Compliance Considerations
Textile chemical buyers increasingly evaluate both product performance and environmental profile. The manufacturer promotes eco-friendly, APEO-free, and formaldehyde-free formulations. These attributes can support textile mills that are working toward restricted substance requirements, retailer chemical policies, and international market expectations.
Environmental compliance should be assessed through current technical documentation, safety data, restricted substance declarations, and customer-specific testing. A product description alone cannot replace formal compliance verification. Textile companies should request the documentation required by their market, certification body, brand customer, or internal chemical management system.
The company identifies OEKO-TEX, ISO 14001, and ISO 45001 among the international standards and management frameworks relevant to its operations and product positioning. OEKO-TEX relates to textile safety and restricted substances, ISO 14001 concerns environmental management systems, and ISO 45001 concerns occupational health and safety management. The precise scope and validity of any certification should be confirmed through current certificates and official documentation.
From a process perspective, the use of a concentrated finishing agent can help reduce packaging, handling volume, and storage requirements when compared with a more dilute product. However, environmental performance also depends on bath concentration, wet pickup, wastewater treatment, energy use, fabric rejects, and the efficiency of the finishing line.
8. Product Advantages for Textile Manufacturers
For textile manufacturers, the value of the product extends beyond the immediate finishing effect. A reliable down-proof and wind-proof agent can help expand the range of cotton fabrics suitable for functional outerwear and filled products. This allows mills to respond to demand for natural fibers while still achieving a level of barrier performance associated with more tightly engineered shell fabrics.
The product can also simplify formulation planning. Its compatibility with non-ionic and weakly cationic auxiliaries makes it possible to develop combined finishing recipes with selected softeners and other compatible products. The important limitation is that anionic auxiliaries must not be included in the same bath. Clear ionicity information helps production teams avoid unsuitable combinations at the recipe-design stage.
The broad dosage range provides flexibility. A mill can begin with a moderate concentration, evaluate air permeability and anti-down performance, and then increase or decrease the dosage depending on the result. This supports a more economical approach than automatically applying a high concentration to every fabric.
The agent’s limited effect on shade and whiteness can also reduce the risk of visual rework. For colored goods, maintaining the target shade is critical. For white goods, preserving brightness and avoiding unwanted discoloration are equally important. The finishing agent is designed to support these requirements when the complete process is correctly controlled.
Finally, the product’s soft film-forming behavior helps address the traditional conflict between protection and comfort. A fabric that passes a laboratory barrier test but feels stiff or noisy may not be acceptable in a finished garment. Maintaining a pleasant hand feel is therefore a significant commercial advantage.
9. Quality Evaluation and Recommended Testing
Product evaluation should include both chemical-bath testing and finished-fabric testing. Before production, the mill should confirm appearance, dispersion, pH, compatibility, and stability of the prepared bath. After finishing, the fabric should be evaluated for air permeability, down-proof performance, handle, shade, whiteness, dimensional stability, and any relevant water-resistance property.
| Evaluation area | Purpose | Suggested control approach |
|---|---|---|
| Bath appearance | Identify precipitation, coagulation, or separation | Inspect before and during application |
| Dispersion stability | Confirm uniform distribution in water | Perform laboratory dilution and observation tests |
| Air permeability | Measure windproof improvement | Use the customer’s approved test method and report conditions |
| Anti-down performance | Determine resistance to feather or down penetration | Test according to the applicable internal or international method |
| Handle | Check softness, drape, and surface feel | Use panel evaluation and, where available, instrumental testing |
| Color and whiteness | Confirm visual stability | Compare treated and untreated standards instrumentally and visually |
| Water performance | Confirm that existing water resistance is maintained | Test spray, hydrostatic, or customer-specific performance as applicable |
| Durability | Assess performance after use or laundering | Apply the required wash and wear simulation before final approval |
Air permeability results should always be reported together with the test standard, pressure difference, sample conditioning, fabric direction, and instrument information. The numerical result can vary significantly when the test conditions change. The same principle applies to anti-down testing: the number of cycles, test apparatus, filling material, movement conditions, and evaluation method should be defined clearly.
Durability testing is also important. A finish may provide excellent initial performance but require adjustment if the final product will be repeatedly washed or subjected to strong mechanical action. The appropriate durability target depends on the end use. A decorative bedding article, a seasonal jacket, and a frequently laundered workwear item may require different levels of retention.
10. How the Product Compares with Alternative Strategies
Textile manufacturers may consider several strategies for reducing down leakage and air permeability. These include increasing fabric density, applying a coating, laminating a membrane, using a tightly spun yarn, adding a resin system, or applying a specialized finishing agent. Each method has advantages and limitations.
Increasing fabric density can improve barrier performance, but it may increase fabric weight, reduce breathability, raise weaving costs, or affect softness. It may also require changes to yarn selection and loom settings. A chemical finish can enhance an existing construction without requiring a complete redesign of the fabric.
Coatings and laminates can provide strong barriers, but they may significantly change hand feel, drape, appearance, recyclability, or moisture behavior. They may also require additional equipment, higher processing temperatures, or more complex quality controls. The Down-Proof & Wind-Proof Finishing Agent is intended to offer a lighter and more flexible surface treatment for applications where a softer textile character is preferred.
Conventional stiffening agents may reduce air movement but can produce an undesirable boardy handle. A specialized polymer complex designed for soft film formation provides a more balanced approach. Its purpose is not simply to make the fabric rigid; it is to create a flexible, dense surface film that supports anti-down and windproof performance.
Silicone softeners can improve handle, but they are not necessarily designed to provide down-proof protection. Conversely, a strong barrier treatment may need to be balanced with a compatible softener. The product’s stated compatibility with non-ionic and weakly cationic auxiliaries allows mills to design a finishing system that considers both performance and feel.
Compared with an unoptimized generic finish, a dedicated down-proof formulation can provide clearer process guidance, more targeted testing, and greater opportunity for technical adjustment. The greatest advantage is achieved when the chemical treatment is integrated with suitable fabric construction and controlled mechanical finishing.
11. Practical Troubleshooting Guide
Uneven Down-Proof Performance
Uneven results may be caused by inconsistent wet pickup, unstable padding pressure, poor bath agitation, fabric width variation, or inadequate cleaning of the machine. The mill should check the padding trough, roller alignment, fabric tension, bath level, and actual add-on across the width.
Insufficient Windproof Performance
If air permeability remains too high, the operator should review fabric density, dosage, wet pickup, setting conditions, and calendering parameters. Increasing dosage alone may not solve the issue if the polymer is not deposited uniformly or if the calendering step is insufficient. A controlled trial that changes one variable at a time is recommended.
Excessive Stiffness
Excessive stiffness may result from an overly high concentration, excessive thermal exposure, excessive calendering pressure, or incompatibility with another auxiliary. The mill can evaluate a lower dosage, adjust the softener package, reduce mechanical compression, or revise the drying and setting profile.
Bath Flocculation or Precipitation
Flocculation is commonly associated with incompatible ionic products, especially anionic auxiliaries. The complete recipe should be reviewed, and the product should not be used in the same bath with anionic chemicals. A separate application stage or a reformulated recipe may be necessary.
Shade or Whiteness Variation
Color variation may be related to uneven application, excessive heat, residual contaminants, or interactions with dyes and other finishing chemicals. The mill should compare untreated and treated laboratory samples, check the thermal profile, and confirm that the fabric has been properly prepared before finishing.
12. Storage, Handling, and Packaging
The product is supplied in 125-kilogram drums. It should be stored in a cool, well-ventilated place. The stated shelf life is six months. Containers should remain properly closed when not in use, and the product should be protected from extreme temperatures, direct sunlight, contamination, and prolonged exposure to unsuitable storage conditions.
Before use, operators should inspect the container and product appearance. If significant separation, coagulation, unusual odor, or other abnormality is observed, the material should be held for technical review rather than introduced directly into production. Storage rotation should follow the first-in, first-out principle whenever possible.
Handling personnel should consult the current safety data sheet and follow the textile mill’s chemical safety procedures. Suitable personal protective equipment, spill control, labeling, and waste management should be used. The product should be handled only by trained personnel familiar with padding chemicals and industrial finishing operations.
13. Applications in Finished Textile Products
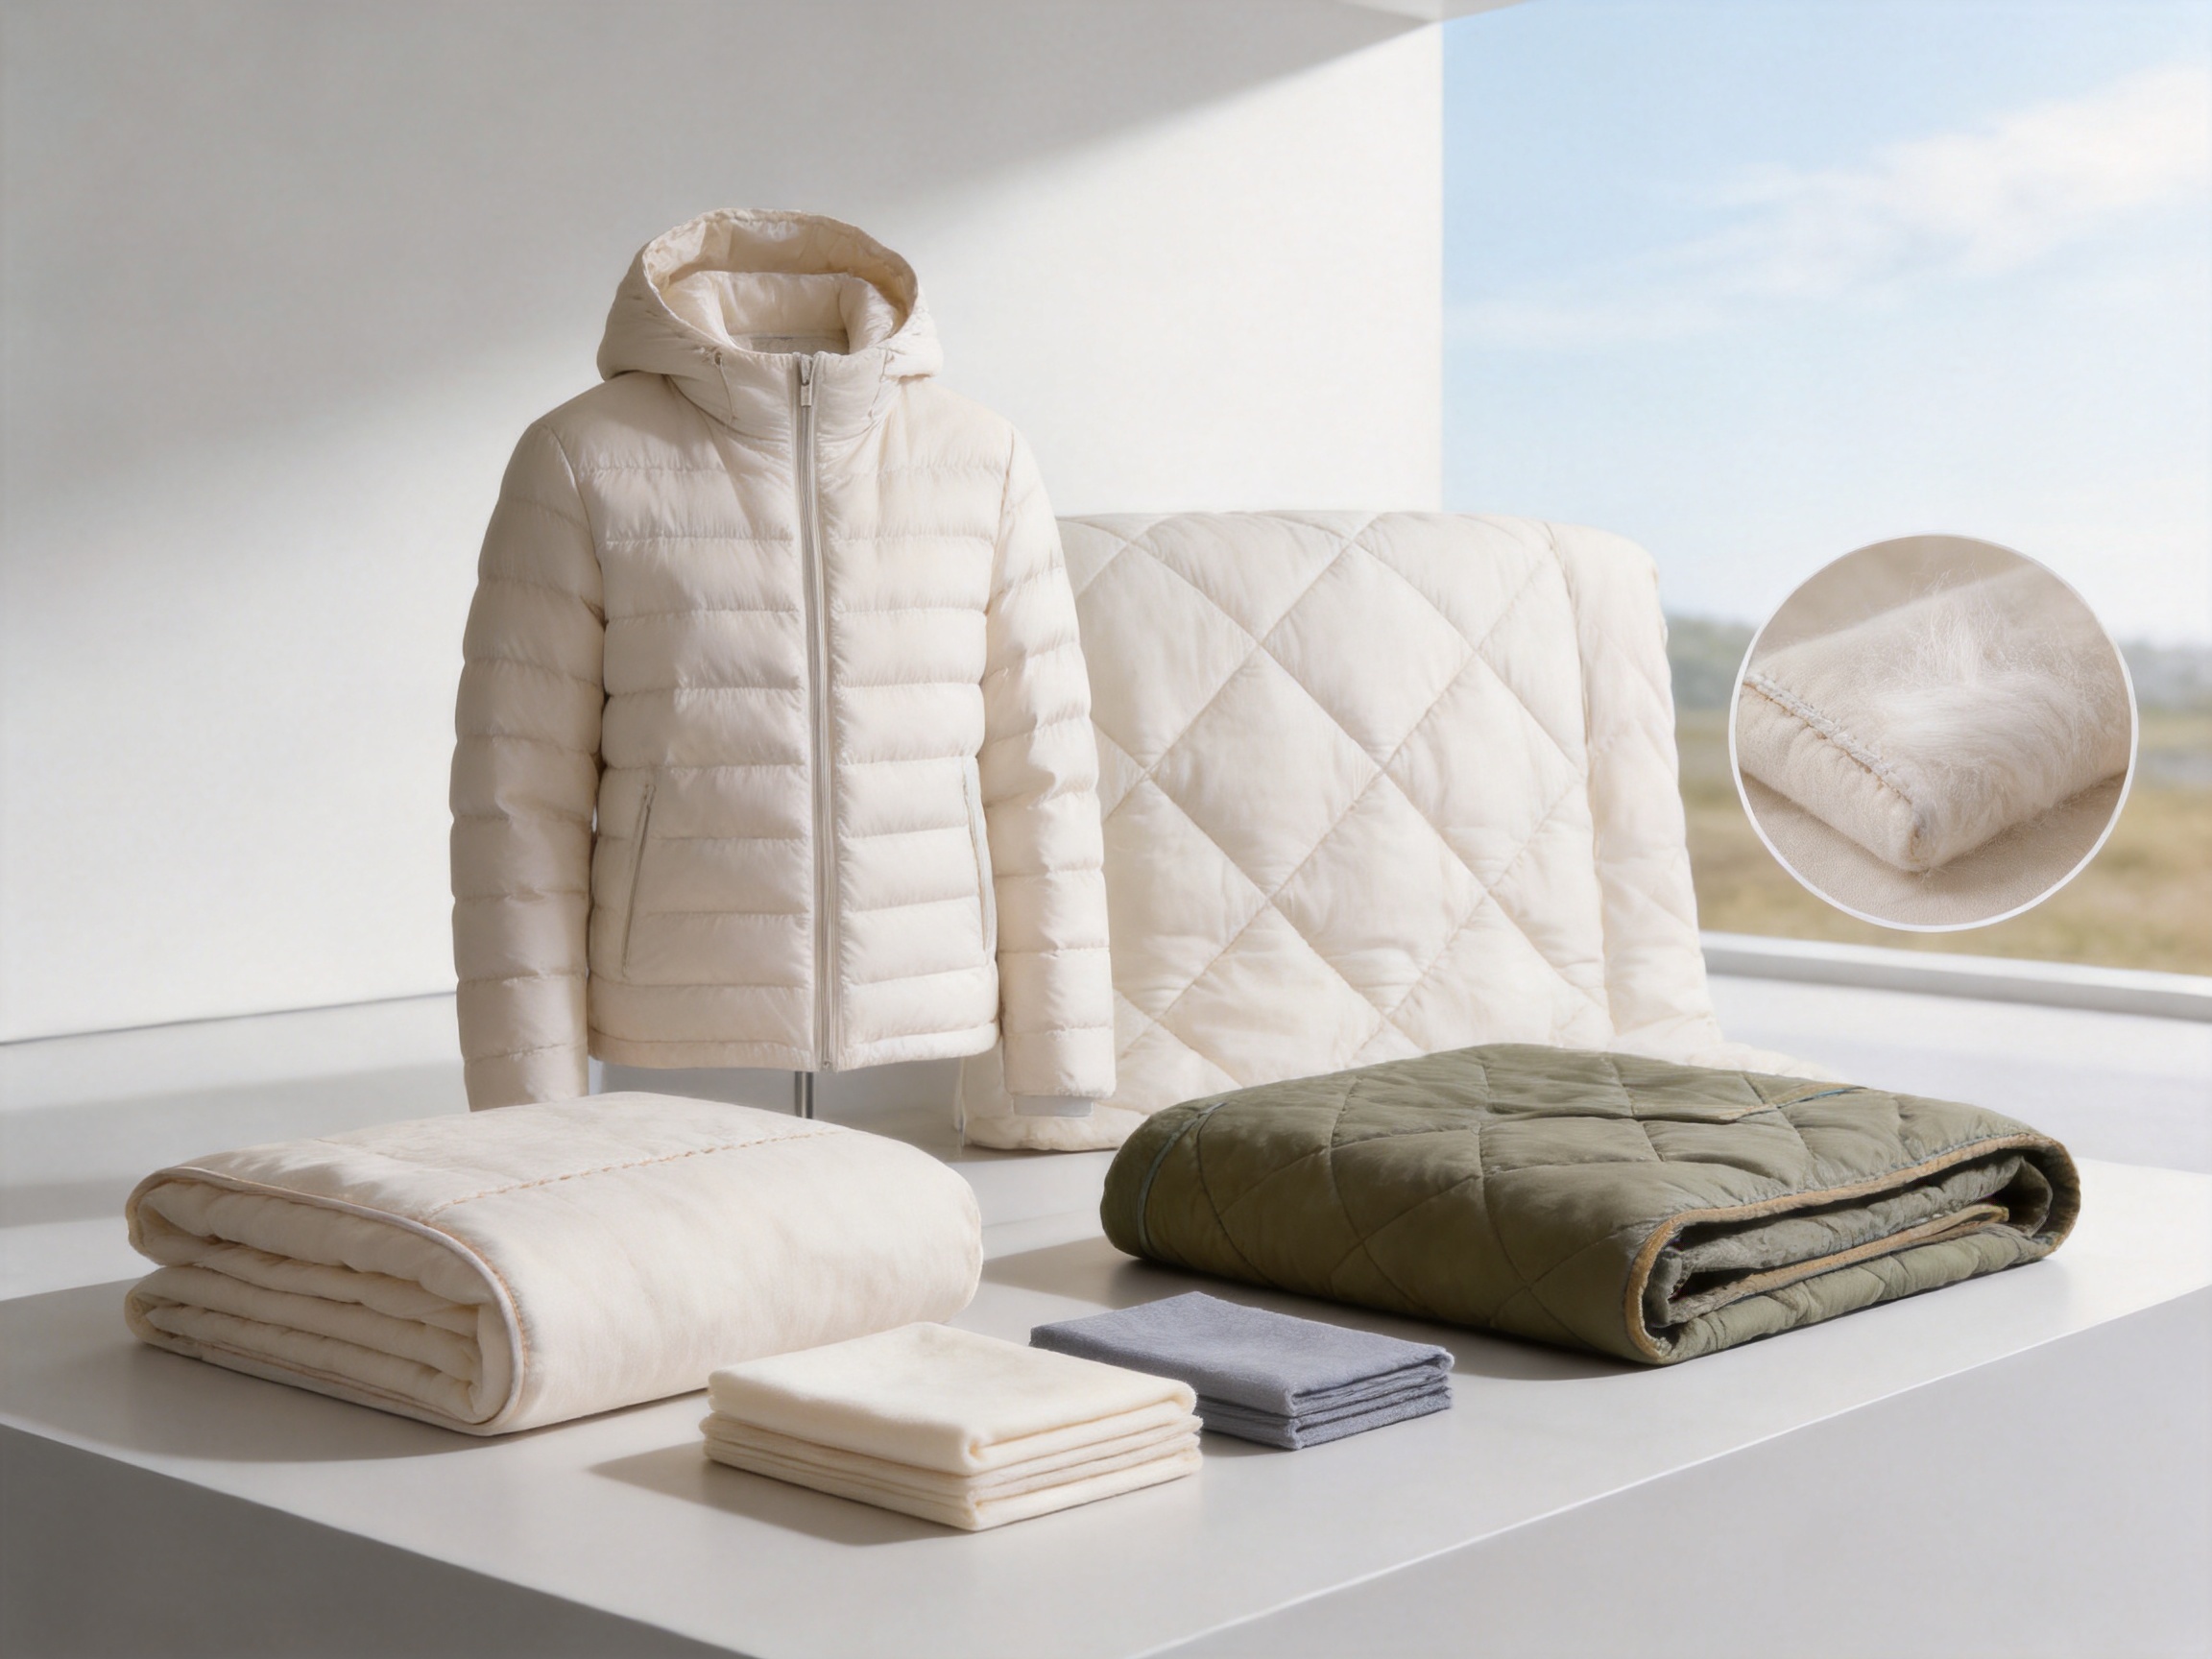
The principal application is down-proof and wind-proof finishing for pure cotton fabrics and cotton-blended fabrics. Potential end uses include cotton outerwear, quilted jackets, lightweight padded clothing, bedding shells, comforters, sleeping products, and other textile articles where feather containment and wind resistance are required.
Pure cotton is especially attractive for consumers who value natural fibers, softness, moisture absorption, and a comfortable skin contact surface. By adding functional barrier performance, the finish can help cotton participate in product categories that traditionally depend on dense synthetic shell fabrics.
Cotton blends may provide additional dimensional stability, strength, drying behavior, or crease resistance. The finishing agent can be evaluated on these substrates, but the blend ratio and fiber chemistry may alter film distribution and handle. A separate laboratory recipe should be developed for each important blend type.
For premium products, the treatment can be combined with careful fabric engineering, quality yarns, controlled weaving, low-impact dyes, compatible softeners, and precision calendering. The result is a more comprehensive performance package rather than a single isolated chemical effect.
14. Why Supplier Collaboration Matters
Textile auxiliaries are most effective when the supplier and mill work together. A product data sheet provides a starting point, but application success depends on the fabric, machinery, water, recipe, and customer standard. Early technical communication can prevent costly trials and production problems.
Before ordering, customers should provide information about fiber composition, yarn count, fabric construction, weight, width, dye class, pretreatment history, target air permeability, anti-down standard, handle requirement, water performance, and laundering expectation. This information allows the supplier to recommend a more appropriate dosage and application process.
Jiangyin Huanan’s product range and formulation capability support cooperation across several stages of textile production. A customer may require only a standard down-proof finish, or may need a complete system involving pretreatment, dyeing compatibility, softening, antistatic performance, water repellency, and fastness improvement. A supplier with a broad auxiliary portfolio can help reduce incompatibility between products from unrelated sources.
Long-term supply relationships also improve consistency. Repeated technical feedback allows the formulation and process to be refined for a specific customer’s equipment and product line. This is particularly valuable for export-oriented manufacturers that must maintain stable results across different seasons, factories, and order volumes.
15. Recommended Implementation Plan for a Textile Mill
A practical introduction program should begin with laboratory screening. Prepare several concentrations within the 50–200 g/L range and apply them to representative fabric samples. Include the planned softener or other compatible auxiliaries, and avoid anionic products in the same bath.
After padding, use a controlled setting process and compare one and two calendering passes. Record wet pickup, drying temperature, setting conditions, calender pressure, roller temperature, and fabric speed. Evaluate air permeability, anti-down performance, handle, appearance, and water performance.
Select the most balanced formulation rather than focusing on a single numerical result. The best recipe should meet the performance target while retaining softness, visual quality, production stability, and reasonable chemical consumption.
The next step is a pilot run on the intended production equipment. Confirm that the laboratory recipe transfers successfully to the full-width machine. Monitor the first and last meters of the run, fabric edges, center, and any areas where tension or wet pickup may change.
Finally, establish a routine control plan. It should define incoming product inspection, bath preparation, addition sequence, padding conditions, machine settings, finished-fabric testing, packaging, and storage. Documented controls make it easier to identify the cause of any future variation.
16. Questions and Answers
Q1: What is the primary function of this finishing agent?
The primary function is to provide down-proof and wind-proof performance for pure cotton and cotton-blended fabrics. It forms a dense cross-linked polymer film on the fiber surface, helping reduce air permeability and prevent down or fine feather materials from passing through the fabric.
Q2: Can it be used on pure cotton fabrics?
Yes. The product is specifically intended for pure cotton as well as selected cotton-blended fabrics. The dosage and process should be adjusted according to yarn count, fabric density, construction, and the required performance level.
Q3: What is the recommended dosage?
The recommended application range is 50–200 g/L. The exact concentration should be determined through laboratory and pilot trials. A higher concentration is not automatically better because excessive add-on may influence handle, appearance, or processing cost.
Q4: Which auxiliaries are compatible with the product?
The product is compatible with non-ionic and weakly cationic auxiliaries when the complete recipe is properly evaluated. It should not be used in the same bath with anionic auxiliaries because ionic incompatibility may cause precipitation or unstable application.
Q5: Will the finish make cotton fabric stiff?
The product is designed to form a soft film and have limited impact on hand feel. Actual handle depends on dosage, fabric construction, wet pickup, setting, calendering, and the selected softener. These variables should be optimized through a controlled trial.
Q6: Does it affect fabric color or whiteness?
The product is designed to have minimal impact on shade and whiteness. Nevertheless, shade and whiteness should be checked on the actual dyed or bleached fabric because the final result may be influenced by dyes, pretreatment residues, other auxiliaries, and thermal conditions.
Q7: Can it be used with waterproof finishes?
The product is described as not affecting waterproof performance. Compatibility should still be confirmed for the specific waterproof agent, application order, and process conditions. Finished fabric should be tested for both water performance and windproof performance.
Q8: What is the recommended process flow?
A typical process is padding with dry fabric feeding, followed by setting and one or two calendering passes. The approximate calendering pressure is 10, and the roller temperature is approximately 80–90°C. Actual conditions should be optimized for the fabric and machine.
Q9: What air permeability can be expected?
The stated target range is approximately 20–30 under relevant test conditions, while anti-down performance can reach below 12 counts. Results depend on fabric construction, dosage, wet pickup, thermal processing, calendering, and the test method. Therefore, customer-specific validation is necessary.
Q10: How should the product be stored?
It should be stored in a cool, well-ventilated place, protected from contamination and unsuitable temperature conditions. The stated shelf life is six months. Containers should remain closed when not in use, and the product should be checked before application.
Q11: What makes the product suitable for industrial textile production?
Its key industrial advantages include easy dispersion in water, a flexible dosage range, compatibility with selected finishing auxiliaries, specialized anti-down and windproof performance, and support from a manufacturer with production capacity, in-house research, quality-control systems, and customized formulation capabilities.
Q12: Should the product be tested after laundering?
Yes, when the finished textile is expected to be washed or exposed to mechanical wear. Laundering and durability tests help determine whether the selected recipe provides sufficient long-term performance for the intended end use.
17. Conclusion
The Down-Proof & Wind-Proof Finishing Agent for Pure Cotton offers a targeted solution for textile manufacturers seeking to combine the comfort of cotton with improved resistance to air penetration and down leakage. Its special high-molecular polymer complex forms a dense cross-linked film on the fiber surface, helping the fabric achieve a lower air permeability index and stronger anti-down performance without unnecessarily sacrificing softness.
The product’s practical advantages include easy water dispersion, a recommended dosage range of 50–200 g/L, limited influence on shade and whiteness, compatibility with non-ionic and weakly cationic auxiliaries, and suitability for padding, setting, and calendering processes. Its use with anionic auxiliaries in the same bath should be avoided.
Manufacturing reliability is supported by Jiangyin Huanan New Materials Technology Co., Ltd.’s long experience in textile auxiliaries, two production plants, reported annual capacity of 60,000 tons, in-house laboratory, professional research and development team, customized formulation capability, and broad product portfolio. These strengths allow the supplier to support not only individual chemical purchases but also more comprehensive textile finishing programs.
For the best results, the finishing agent should be evaluated as part of an integrated system that includes fabric construction, wet pickup, thermal treatment, calendering, compatible softeners, and finished-fabric testing. When these factors are controlled, the product can help textile mills develop comfortable, attractive, and functional cotton fabrics for down-filled apparel, bedding, outdoor products, and other performance-oriented applications.
References
1. Technical product information for Down-Proof & Wind-Proof Finishing Agent for Pure Cotton, including composition, application range, compatibility, packaging, and storage guidance.
2. Jiangyin Huanan New Materials Technology Co., Ltd. company information concerning textile auxiliary research, production capacity, product categories, and customized formulation services.
3. General textile finishing principles concerning padding, wet pickup, thermal setting, polymer film formation, and calendering.
4. General textile testing principles for air permeability, down-proof performance, color stability, handle, water resistance, and laundering durability.
5. International textile chemical management and environmental management references, including OEKO-TEX, ISO 14001, and ISO 45001 frameworks.
Product: Down-Proof & Wind-Proof Finishing Agent (Pure Cotton)
Contact us
huanannewmaterials@gmail.com
-
 Phone: +86 - 13861620767
-
 Fax: +86-0510-86200939
-
 298 Hongxing Road, Huashi Town, Jiangyin City, Wuxi City, Jiangsu Province, China
Product links
Mobile App
Copyright © Jiangyin Huanan New Materials Technology Co., Ltd. All Rights Reserved
-
huanannewmaterials@gmail.com
-
-
-
+86 - 13861620767